
A 3/8-inch UHMW blank exploding on a press brake bed sounds exactly like a 12-gauge shotgun fired inside a steel dumpster. My lead operator simply stared at the white plastic fragments scattered across the diamond plate. He had done precisely what twenty years of experience had taught him: increase the tonnage. But UHMW does not respond to brute force. It stores that energy—until the moment it violently releases it.
Related: Press Brake Tooling Rack
Related: How to Bend Stainless Steel Sheet
The Cold-Forming Trap: Why Your Best Metal-Bending Instincts Ensure Failure
Think of mild steel as a dense, stubborn block of clay. When you drive a punch into it, the clay yields. It displaces, retains the new shape, and accepts the change. You are in control, the press brake is your hammer, and the metal is the anvil.
Now imagine swinging that same hammer at a tightly wound bundle of a billion heavy-duty rubber bands. You can compress that bundle flat under a hundred tons of pressure. It may appear flat while the ram is down. But the instant you release the pedal, those rubber bands will fight aggressively to return to their original form. Push them too far, and they do not merely deform—they snap.
Treating Polymer Chains Like a Crystalline Lattice
Examine a piece of 10-gauge cold-rolled steel under a microscope and you will see a clean, orderly grid—a crystalline lattice. When you bend metal, you are literally sliding planes of atoms past one another until they lock into a new arrangement. That is plastic deformation. You have forced a permanent yield.
UHMW has no orderly grid. It resembles a tangled, chaotic bowl of microscopic spaghetti. Those polymer chains are extremely long—that is the source of the "ultra-high molecular weight" designation, and it is precisely why the material can absorb a sledgehammer blow that would significantly dent steel. But when you press a standard V-die into cold UHMW, you are not sliding neat rows of atoms. You are stretching those tangled chains against their nature. They do not want to slide; they want to snap back. Metal fabricators are accustomed to materials that eventually yield. UHMW does not. It possesses a persistent elastic memory.
Why More Tonnage and Sharper Dies Only Speed Up Stress Whitening
When a cold-bent part springs back 30 degrees, the natural reaction is to apply more force. You switch to an acute punch, narrow the V-die, and increase the tonnage to coin the radius. With aluminum, this sets the bend. With UHMW, you have just ensured its failure.
Observe the outside radius of the plastic as the punch reaches bottom. A milky, opaque line spreads across the bend axis. This is stress whitening. It is not merely cosmetic; it is visible evidence of micro-crazing. You are physically pulling the polymer chains apart. Because the material’s stiffness is extremely low—about 0.8 GPa compared to steel’s 200 GPa—the machine does not sense resistance the way it does with metal. The ram continues to advance, and the polymer chains continue to stretch until they rupture internally. The sharper the die, the more intensely you focus that tearing force into a single microscopic pivot point.
The Illusion of Success: The Crack That Appears Three Days Later
Sometimes, the shop floor deceives you. You remove the part from the brake, overbend it by 40 degrees to offset springback, and verify it with a protractor. Exactly 90 degrees. You stack it on a pallet, ship it to the customer, and congratulate yourself for mastering the problem.
Seventy-two hours later, the phone rings. The parts are breaking in the field under minimal load.
This is the fundamental trap of cold-forming heavy plastics. When you impose a bend without heat, you have not actually relieved the material. You have only trapped that kinetic energy within a stretched, damaged molecular structure. The polymer chains remain locked in a high-tension state, constantly trying to return to flat. Over hours and days, that internal stress exploits the micro-fractures created during bending. The material quite literally pulls itself apart from the inside out. To properly form UHMW, you must stop fighting the rubber bands and start calming them.
Material Memory vs. The Ram: What UHMW Is Actually Doing
I recall the first time I attempted to air-bend a 1/2-inch sheet of UHMW over a 4-inch V-die. I lowered the punch, expecting the familiar resistance of material yielding to the machine. Instead, the ram traveled two full inches into the die, and the tonnage display barely rose above zero. The sheet simply arched into the void like an industrial trampoline. When the ram retracted, the plastic snapped back to perfectly flat, openly defying the hundred-ton machine above it. That is the precise moment you understand that the press brake, as a mechanical force multiplier, is entirely the wrong tool for the job unless you change the physics involved.
The stiffness gap: Why UHMW flexes where mild steel would yield
In metalworking, stiffness and yield point are closely connected. Mild steel has a stiffness—its Young's modulus—of about 200 GPa. When a punch strikes it, the material resists immediately, the tonnage spikes, and the crystalline lattice shears into a permanent new angle.
UHMW is around 0.8 GPa. It is 250 times less stiff than steel.
When the punch contacts UHMW, the material does not resist enough to create a localized yield at the bend line. Instead, it spreads the stress across the entire span of the die opening. The ram is applying force, but the material is merely flexing, absorbing the kinetic energy by temporarily increasing the spacing between its molecular chains. You are not forming a flange; you are simply pulling a very tight bowstring. How do you create a permanent bend in something that refuses to hold a permanent crease?
Why the part persistently tries to return to a flat sheet
If you hold the ram at the bottom of the stroke, you might think you have succeeded. But UHMW’s molecular structure is dominated by highly crystalline regions connected by amorphous, highly flexible chains. When you force it cold into a V-die, those amorphous chains are stretched to their absolute physical limit.
They are filled with potential energy.
Because there is no crystalline shear as in metal, there is no "reset" of the material’s baseline shape. The polymer’s baseline remains completely flat. The moment you release the clamping pressure, those stretched chains rapidly contract to their lowest energy state. A 90-degree bend will spring back to 160 degrees before you can even measure it with calipers. If you attempt to overbend it cold to compensate, you simply break the chains, leading to stress whitening and delayed cracking that ruins parts in service. So if mechanical force results only in temporary tension or permanent damage, what actually alters the polymer’s baseline shape?
Reframing the machine: Using the brake for thermal guidance, not brute force
The answer is heat, but not in the way a blacksmith uses a rosebud torch. You must raise the UHMW to its softening point—typically around 260°F to 280°F.
Within this specific thermal window, the polymer’s rigid crystalline regions begin to melt just enough to allow the tangled amorphous chains to slide past one another without breaking. You are, in effect, chemically sedating the rubber bands. At this stage, the press brake’s role changes completely. It is no longer a hammer forcing yield; it becomes a thermal fixture. You lower the ram onto the heated plastic, overbending it by a carefully calculated margin to account for inevitable thermal shrinkage, and then you do the hardest thing for a metal fabricator to do: you keep the ram down.
You maintain pressure while the material cools below 200°F.
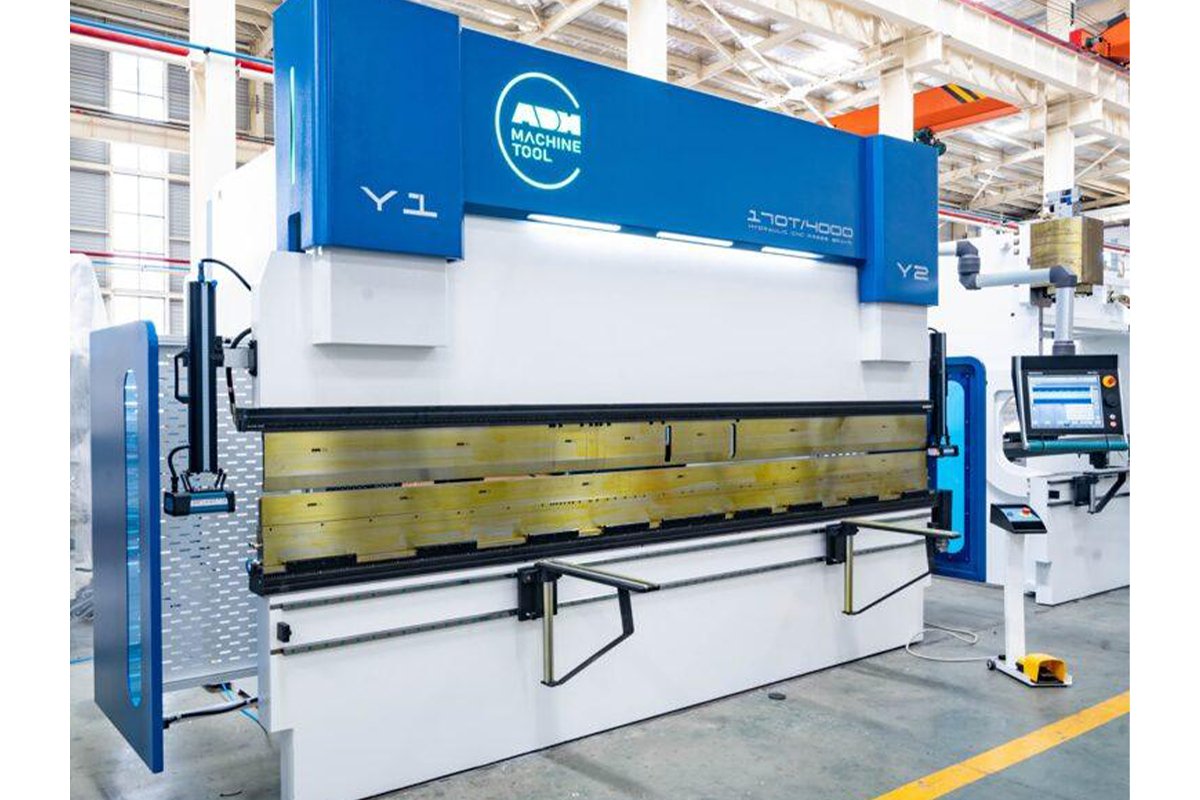
You are forcing the polymer chains to solidify in their new, relaxed positions. The brake is not performing the bend; the heat is, and the brake merely controls the geometry as the plastic sets. In this context, precision ram positioning, repeatable stroke control, and programmable dwell become far more important than raw tonnage—capabilities built into a modern CNC press brake from ADH Machine Tool, whose fully CNC-based systems are designed for high-end bending applications where accuracy and consistency define the outcome. But if the plastic is now hot, soft, and pliable enough to assume a new shape, what happens when your standard, razor-sharp gooseneck punch presses into it?
Retooling the Bed: Why Standard Metal Tooling Destroys Polymers
You remove a 1/4-inch sheet of UHMW from the oven at 270°F. It feels heavy and inert in your hands, like a thick slab of medium-rare steak. You position it over the die, lower a standard acute punch with a 1/32-inch tip, and watch the ram press into the material. Because the plastic is hot and soft, the machine senses little resistance. But you are not forming a part—you are creating a very expensive, very slow guillotine. The sharp punch tip displaces the softened polymer, driving a deep crease into the inside radius. In metal, this is called a crisp bend line. In polymers, it is a significant stress riser. As the part cools, the molecular chains attempt to shrink, but that sharp crease acts like a pre-cut tear line, ensuring the flange will snap off the first time a forklift strikes it. If a sharp punch functions like a knife on heated plastic, what geometry is actually required to bend it safely?
The punch radius rule: At what thickness ratio does UHMW simply snap?

In sheet metal, you can routinely use a punch radius equal to the material thickness (1T), or even 0.5T when coining mild steel. UHMW follows a completely different set of geometric limits. When you bend a sheet of plastic, the material on the outside of the radius must travel farther than the material on the inside. If you apply a 1T punch to UHMW, you concentrate all that stretching into a microscopic surface area. The outer polymer chains thin, stretch beyond their elastic limit, and micro-fracture—even when heated.
To keep the outer fibers intact, you must distribute that stretch across a much wider arc.
The baseline guideline for heavy plastics is a minimum punch radius of 1.5T to 2T. If you are forming 1/4-inch UHMW, you need a 3/8-inch or 1/2-inch bullnose punch. This larger radius compels the material to wrap rather than crease, spreading the tensile load across millions of polymer chains instead of concentrating it on a few thousand. However, while a bullnose punch addresses tearing on the top surface of the sheet, what is the standard tooling doing to the bottom?
Why standard V-dies and goosenecks create invisible internal stress
Consider a standard steel V-die. It consists of two hard, rigid shoulders separated by a gap. When you press cold steel into that gap, the metal slides over the shoulders and yields in the center. When you press hot, low-friction UHMW into the same space, the physics work against you.
The heated plastic does not roll smoothly over the die shoulders. It drags and extrudes.
Because the UHMW is softened, the cold steel shoulders dig into the bottom surface of the sheet as it is forced downward. More critically, the void at the center of the V-die provides no support to the apex of the bend. Instead of folding cleanly, the hot plastic bulges into the empty space of the die, causing localized thinning at the precise point where the part requires the most structural integrity. The "invisible stress" operators report is not always molecular memory—often, it is the physical damage from dragging soft plastic over hard steel edges while the center of the bend extrudes into open air. How do you support a material that tends to flow away from pressure?
Urethane bottom dies: A high-end luxury or a strict requirement?
If you are bending 1/8-inch UHMW prototypes and reduce your tonnage to a minimum, you can sometimes get by with a heavily polished, oversized metal V-die. However, for production runs or anything thicker than 1/4-inch, a urethane bottom die is a strict requirement.
You replace the steel V-die with a steel channel filled with a solid urethane pad.
When the bullnose punch drives the hot UHMW into the urethane, the pad functions as an incompressible hydro-cushion. It displaces around the punch, pressing the hot plastic firmly against the tooling. There are no hard steel shoulders to gouge the surface, and more importantly, there is no void. The urethane delivers continuous, uniform upward pressure against the outside radius of the bend, physically preventing the hot plastic from bulging or thinning. You are no longer air-bending; you are effectively hydro-forming the polymer. But now that we have a bed designed to safely support hot plastic, how do we ensure the core of that plastic is actually at the correct temperature without melting the surface into a puddle?
The Thermal Guidance Protocol: Executing the Bend
UHMW has a thermal conductivity of about 0.4 W/(m·K)—less than one-hundredth that of carbon steel. If you handle it like metal and blast the bend line with an acetylene torch or an overpowered strip heater, the surface turns into a sticky, bubbling mass while the core remains rigid and cold. When the ram descends, the cold core fractures, and the melted surface adheres to your new urethane die. You must treat the plastic like a thermal battery. The objective is a uniform 260°F to 280°F throughout the entire cross-section, which requires managing time as carefully as temperature.
For fabricators who want detailed machine parameters, CNC control capabilities, and tooling configurations designed to manage controlled heating and precision bending, ADH Machine Tool provides comprehensive technical documentation across its fully CNC-based bending systems. You can download the technical brochures and specification sheets here to review concrete data on machine control, automation options, and high-end bending solutions suited for temperature-sensitive materials.
The thermal sweet spot: Softening the core without melting the surface (Oven vs. Strip Heat)
If you place a 15-inch UHMW blank in a convection oven set to 275°F, you achieve complete core heat penetration. However, you also induce significant thermal expansion. UHMW expands at roughly five times the rate of steel. That 15-inch part can increase in length by nearly 3/16 of an inch during heating. If it contains pre-drilled bolt holes or tight-tolerance cutouts, their positions will shift, and they will not return precisely to their original centers after cooling.
For precision components, localized strip heating is required.
A strip heater cannot be rushed. Dual-sided, temperature-controlled elements set to 300°F are necessary, with a soak time of 15 to 20 minutes per quarter-inch of thickness—the appearance of a translucent bend line indicates that the core is ready. The surface temperature never exceeds the degradation threshold, but the extended dwell allows heat to gradually penetrate into the core.
Time-to-brake: The critical window between the heat source and the ram
The moment you remove the blank from the heat source, timing begins. Ambient shop air immediately starts drawing thermal energy from the surface. You have a working window of approximately 30 to 45 seconds before the outer skins fall below 200°F. If the skins cool excessively, they regain stiffness and will micro-fracture when stretched over the bullnose punch, even if the core remains fully softened.
This requirement determines your shop floor layout.
The heating station must be positioned within two steps of the press brake. Operators cannot be walking across the shop, talking with the forklift driver, or adjusting backgauges. The brake must be preset, the urethane die cleared, and the stops locked before the plastic leaves the heat source. The movement must be synchronized: grab, position, press the pedal.
The 40-degree overbend: Mathematically compensating for extreme springback

You align the bend line precisely, the core reaches 270°F, and the ram descends. If you need a 90-degree bracket and you drive the punch to 90 degrees, the result will be a 130-degree ramp. Even when heated, UHMW retains a strong elastic memory. The polymer chains are relaxed, but they are not eliminated.
Given that ADH Machine Tool's product portfolio is 100% CNC-based and covers high-end scenarios in laser cutting, bending, grooving, shearing, for teams evaluating practical options here, Electric Press Brake is a relevant next step.
To achieve a 90-degree angle, you must drive the punch to an included angle of 50 degrees.
This 40-degree overbend pushes the polymer chains well beyond their neutral state. It stretches the outer fibers and compresses the inner fibers to such an extent that when they attempt to recover, they exhaust their stored energy exactly at 90 degrees. Accomplishing this demands deep, specialized tooling clearances. Standard punches will bottom out on the flanges before reaching a 50-degree included angle. A tall, narrow gooseneck punch with a large bullnose integrated at the tip is required to clear the sweeping wings of the overbent plastic.
For example, ADH Machine Tool's product portfolio is 100% CNC-based and covers high-end scenarios in laser cutting, bending, grooving, shearing; ADH Machine Tool operates more than 50 sales and service points in China and overseas; for teams evaluating practical options here, Tandem Press Brake is a relevant next step.
Dwell time and constraint: Quenching vs. air-cooling to lock the angle
Reaching the 50-degree overbend is only half the task; the other half is restraining the material. If you pull the ram back right away, the heated plastic will spring open dramatically because the molecular chains remain mobile. You must keep the ram engaged, holding the plastic firmly in the urethane die until the core temperature falls below 160°F.
In ambient air, a 1/2-inch sheet clamped in the brake can take up to ten minutes to cool.
No production shop can accommodate a ten-minute cycle. Operators often attempt to cut corners by spraying the clamped part with water or blasting it with compressed air. Rapid quenching causes the outer surfaces to contract immediately while the core remains hot, creating severe internal stress that will distort the flange as soon as you release the ram. Instead, use an aluminum chill block. A thick piece of cold aluminum placed against the inside radius extracts heat quickly but uniformly through conduction, reducing dwell time to about two minutes without shocking the polymer. You release the ram, the part springs back 40 degrees, and stops precisely at a perfect right angle. But what if your calculations are exact, your heat is correct, and the material still will not hold its shape?

The Boundary Check: When to Step Away from the Press Brake Entirely
You did the calculations. You reached the 270°F sweet spot. You overbent to 50 degrees, cooled it correctly with an aluminum block, and released the ram to see a flawless 90-degree angle. Then you place the part on the inspection table, and over the next three hours, it slowly and almost mockingly opens up to 110 degrees. Why? Because you brought a press brake to a volume fight.
In metalworking, if a plate is thick and resistant, you simply purchase a larger machine with more tonnage.
In heavy plastics, tonnage has no relevance. When the material’s cross-section becomes too massive, the sheer bulk of the internal polymer chains—those billions of entangled rubber-band-like strands—overpowers the heat-softened outer layers. The internal stress does not just oppose the bend during the cycle; it continues to fight back long after the part has cooled, gradually pulling it out of tolerance. You did not fail at bending; you simply reached the material’s absolute physical limit of elastic memory. So where is that physical boundary?
At What Thickness Does Forming Become Structurally Irresponsible?
In sheet metal, "too thick" means you need a larger V-die and a 1,000-ton Cincinnati. In heavy plastics, "too thick" means you are actively compromising the part’s structural integrity. For UHMW, that boundary is effectively marked at half an inch. Once you move into 5/8-inch or 3/4-inch thickness, the thermal physics we depend on begin to fail.
Recall that extremely poor thermal conductivity.
To raise the core of a 3/4-inch sheet to 270°F without turning the surface into a puddle, you must soak it so long that the material starts to degrade and oxidize. If you shorten the soak time to protect the surface, you end up bending a cold, rigid core wrapped in heated outer layers. The exterior stretches, but the interior develops micro-fractures. Those hidden fractures behave like a zipper waiting to split apart the moment the part experiences impact in service. You are not producing a heavy-duty bracket; you are creating a time bomb. But if the drawing specifies a 3/4-inch angled wear pad and the press brake is not an option, how do you actually manufacture it?
Routing and Welding vs. Bending: Preserving the Material’s Wear Resistance
Engineers specify UHMW for one main reason: it withstands extreme abuse. It is used to line coal chutes and grain hoppers because its slick, dense molecular structure resists abrasion that would wear through carbon steel in a week. When you force a bend in thick UHMW, you stretch and thin the outer radius, undermining the very wear properties the engineer intended to preserve.
At that point, you have to set aside your pride, step away from the brake, and move to the CNC router.
Rather than bending a 3/4-inch sheet, you machine two separate plates with precisely matched bevels. Then you bring out the extrusion welder. Plastic welding is not like running a TIG bead on stainless steel; you are injecting molten UHMW into the joint, fusing the plates together at a molecular level. A properly extruded corner joint in thick UHMW preserves 100% of the material’s original thickness and wear resistance at the apex. It takes more time, and it can feel like a setback to someone who spent twenty years forming metal. But the finished part will endure a decade of rock crushing instead of failing during its first shift. So how do you prevent yourself from making the wrong decision before the first sheet is even cut?
The fabricator's pre-job checklist to avoid reverting to metal logic
The most difficult habit to break is not physical but psychological. When an urgent job hits the floor, your mind defaults to the metal-based thinking that sustained your career for decades. You look at a drawing, see an angle, and immediately begin calculating V-die openings. You need a firm pause, but instead of a laminated safety poster on the wall, that checklist must activate in your mind the moment you step up to the pedal.
I still catch myself doing it. I’ll be at the brake, holding a slick sheet of UHMW, feeling the 270-degree heat radiating from the bend line through my leathers. The old metalworker in me wants to slam the pedal, drive it into a sharp die, and let the tonnage handle the rest. Then the mental filter engages: Is this under half an inch? Yes. Did I pressure the engineer into approving a broad bullnose radius? Yes. Are my aluminum chill blocks positioned on the bed, ready to lock this polymer in place?
Only when the physics align do I lower the ram. Steel yields to force, but UHMW responds only to thermal control. When you stop trying to overpower a polymer chain and instead work with its persistent memory, the frustration disappears. You are no longer a metalworker struggling with plastic; you become a fabricator capable of forming anything.
Given that ADH Machine Tool maintains a complete quality control system and disciplined production process, if the next step is to speak with the team directly, contact us fits naturally here.

















 English
 العربية
 বাংলা
 Български
 Čeština
 Dansk
 Nederlands
 Deutsch
 Suomi
 Français
 Ελληνικά
 עִבְרִית
 हिन्दी
 Magyar
 Bahasa Indonesia
 Italiano
 日本語
 Қазақ тілі
 한국어
 Bahasa Melayu
 Norsk bokmål
 فارسی
 Polski
 Português
 Português do Brasil
 Română
 Русский
 Српски језик
 Slovenčina
 Español de México
 Español
 Svenska
 Kiswahili
 தமிழ்
 Türkçe
 ไทย
 Tagalog
 Українська
 Tiếng Việt
 اردو
 简体中文
 香港中文
 繁體中文