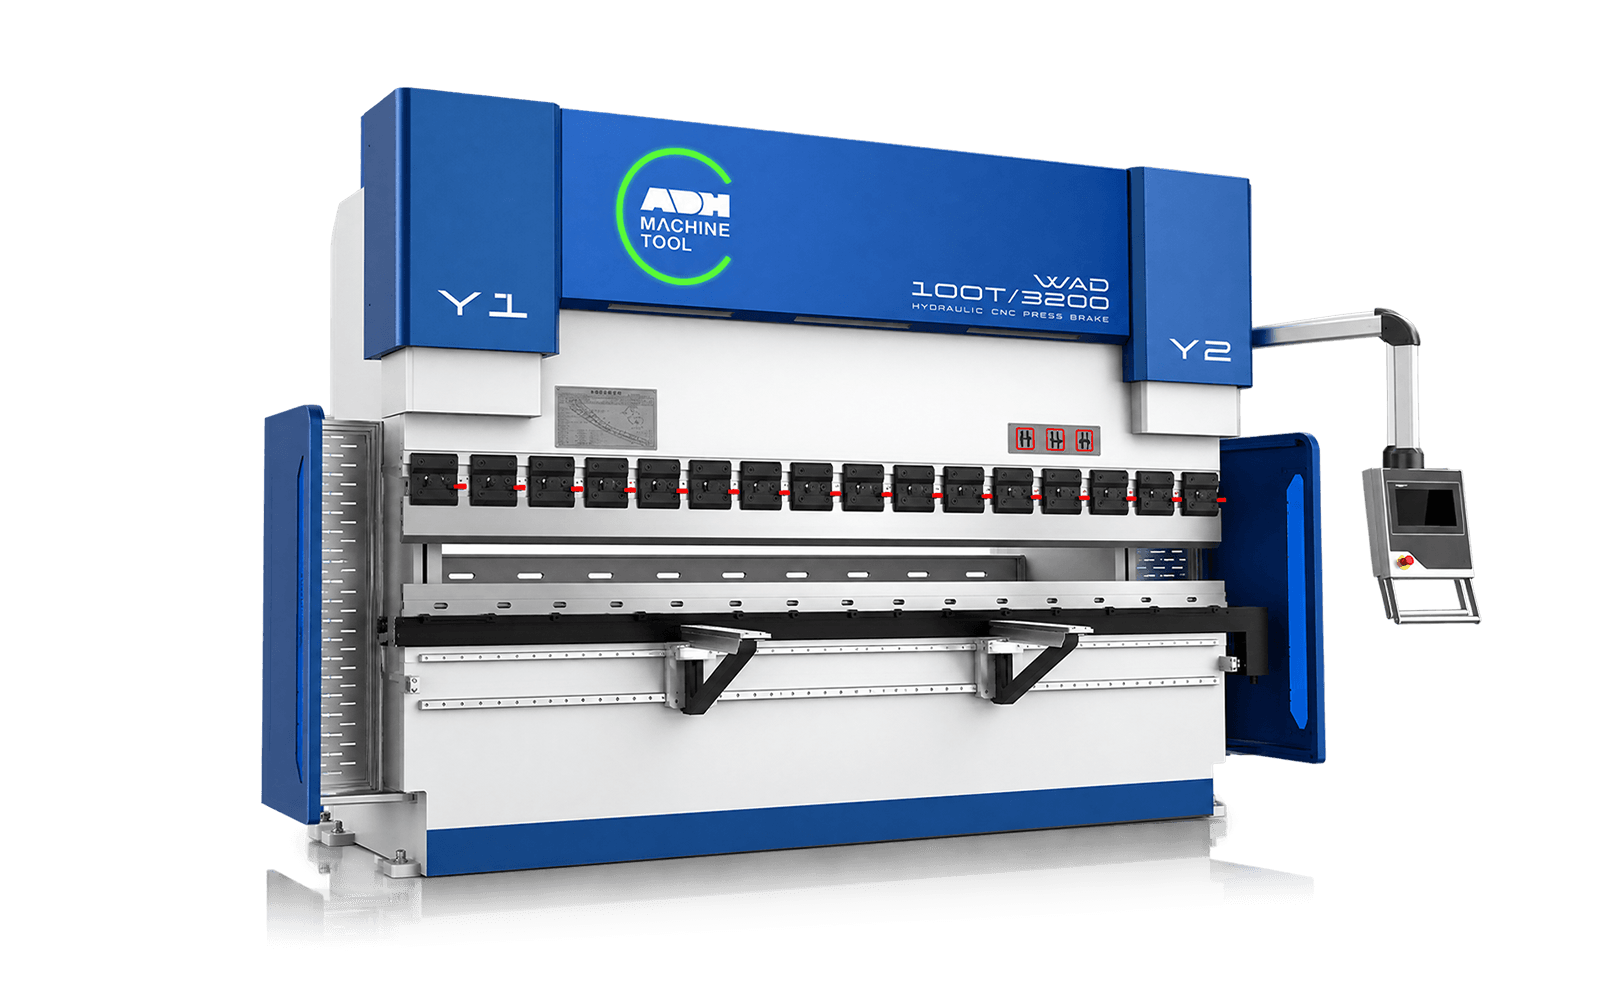
Bend varied parts
Press brakes
For brackets, profiles and folded parts. Start with the bend shape, tooling access and required force.
How to choose a press brake
No languages found. Try another name or language code.
Machine selection
Compare machines by the parts you make, the process they need and your production volume.
01 / Choose a process
Match the operation to your workpiece. One finished product may need both cutting and forming equipment.
Bend varied parts
For brackets, profiles and folded parts. Start with the bend shape, tooling access and required force.
How to choose a press brake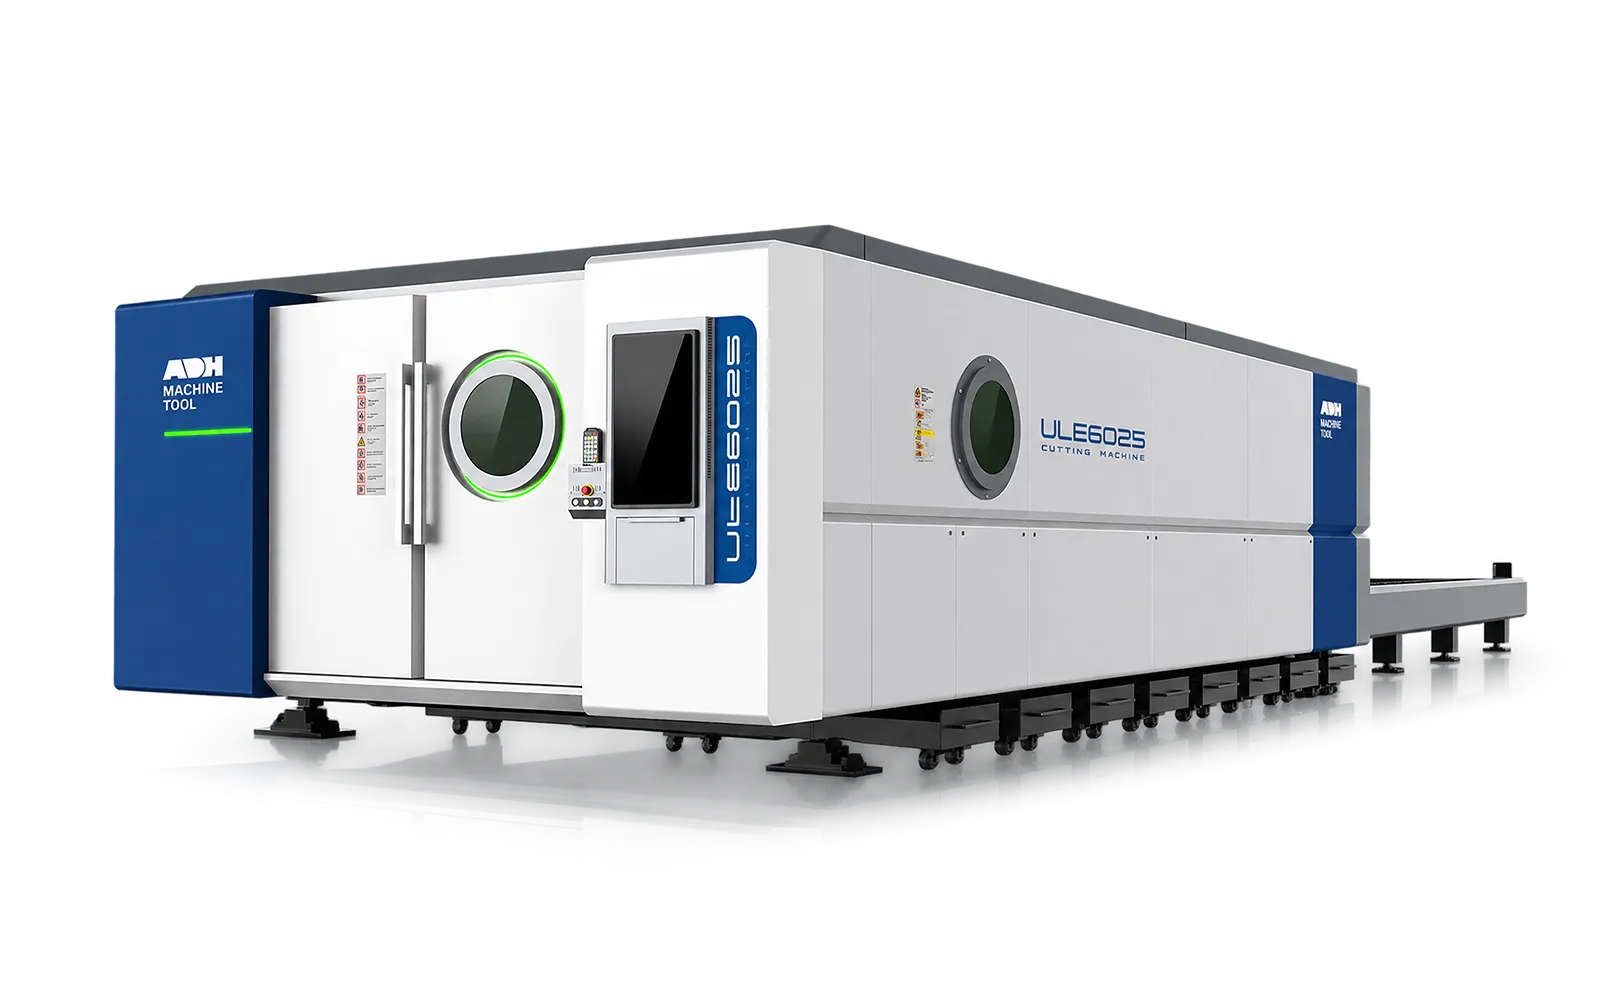
Cut outlines and holes
For sheet, tube and profile features. Choose the workpiece format first, then the process and handling setup.
How to choose a laser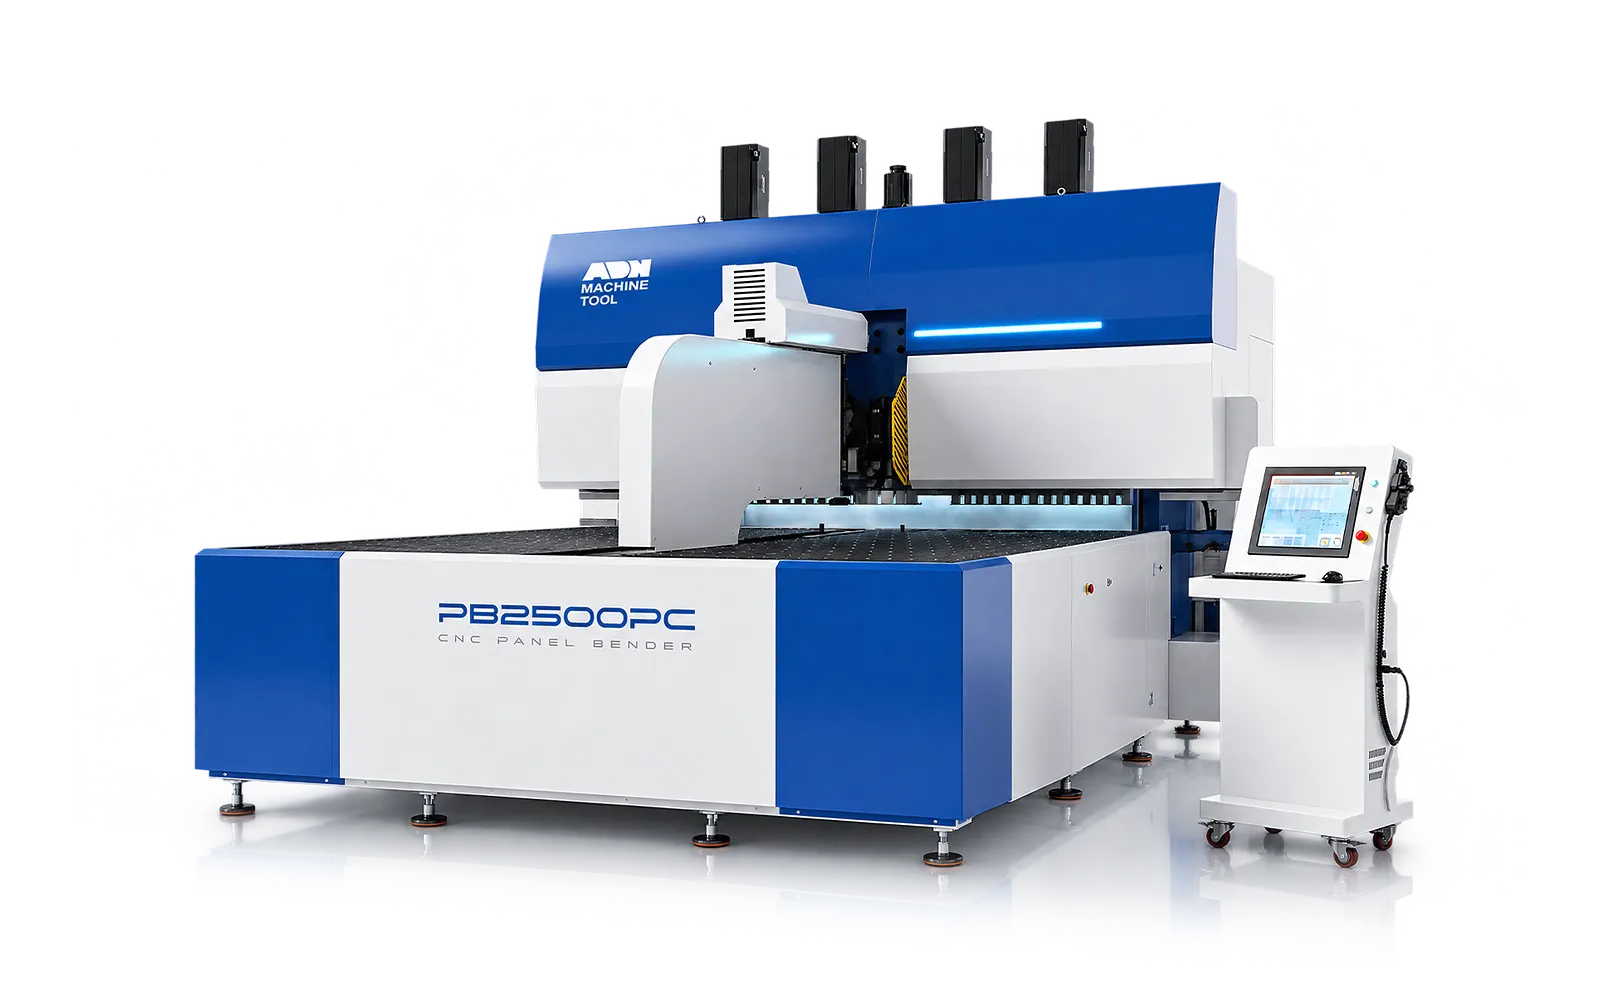
Form multi-sided panels
For compatible doors, trays and panels. Check flanges, clamping and part clearance before comparing tool changes.
How to choose a panel bender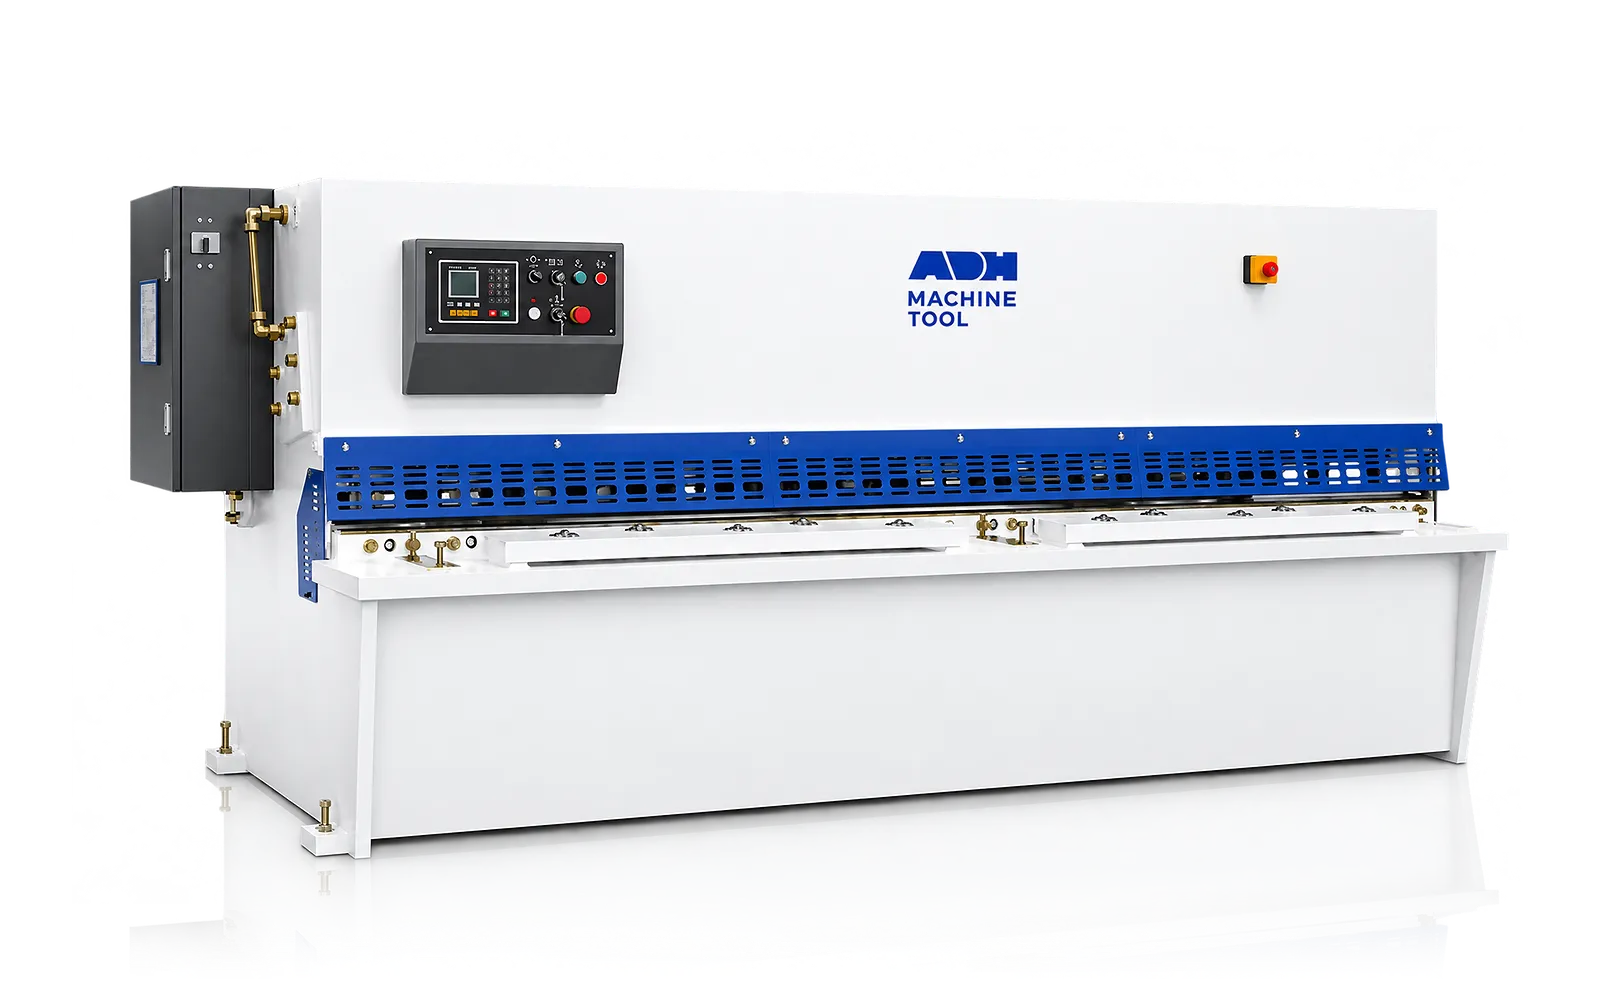
Cut straight-edged blanks
For straight cuts and repeated strips. Material strength, cut length and sheet support guide the choice.
How to choose a shear02 / Compare the process
Choose by the work that must be completed. Compare geometry first, then the complete cycle and changeover.
Compare
Press brake
Panel bender
Start here
Press brake
Varied brackets, profiles and folded parts where the selected punch, die and bend sequence can reach every feature.
Panel bender
Compatible doors, trays and multi-sided panels where clamping and programmed panel movement fit the geometry.
Check first
Press brake
Force, bend length, tool clearance, backgauge references and support through the complete bend sequence.
Panel bender
Material range, panel size, flange heights, return bends, clamping zones and finished-part removal.
Compare the job
Press brake
Include programming, tool setup, part turning and loading. Check regular work and difficult exceptions.
Panel bender
Include setup and loading. PB-M changes segmented tooling manually; PB-A selects upper-tool length automatically.
Both processes can serve different parts in the same assembly. A high-mix workload alone does not determine the machine.
Compare
Fiber laser
Hydraulic shear
Required features
Fiber laser
Outlines, holes and profiled features in compatible sheet, tube or profile workpieces.
Hydraulic shear
Straight-edged sheet or plate blanks and repeated strips.
Check the result
Fiber laser
Material, thickness, small features, gas, edge condition and preparation for the next operation.
Hydraulic shear
Material shear strength, cut length, squareness, burr, distortion and support for narrow strips.
Compare the job
Fiber laser
Include nesting, cutting, loading, part removal and any edge finishing.
Hydraulic shear
Include positioning, cut sequence, collection and any separate work needed to create holes or contours.
Compare the whole route to the finished blank, including any downstream operations.
03 / Narrow your shortlist
Open your process checklist, then compare models and specifications on the product pages.
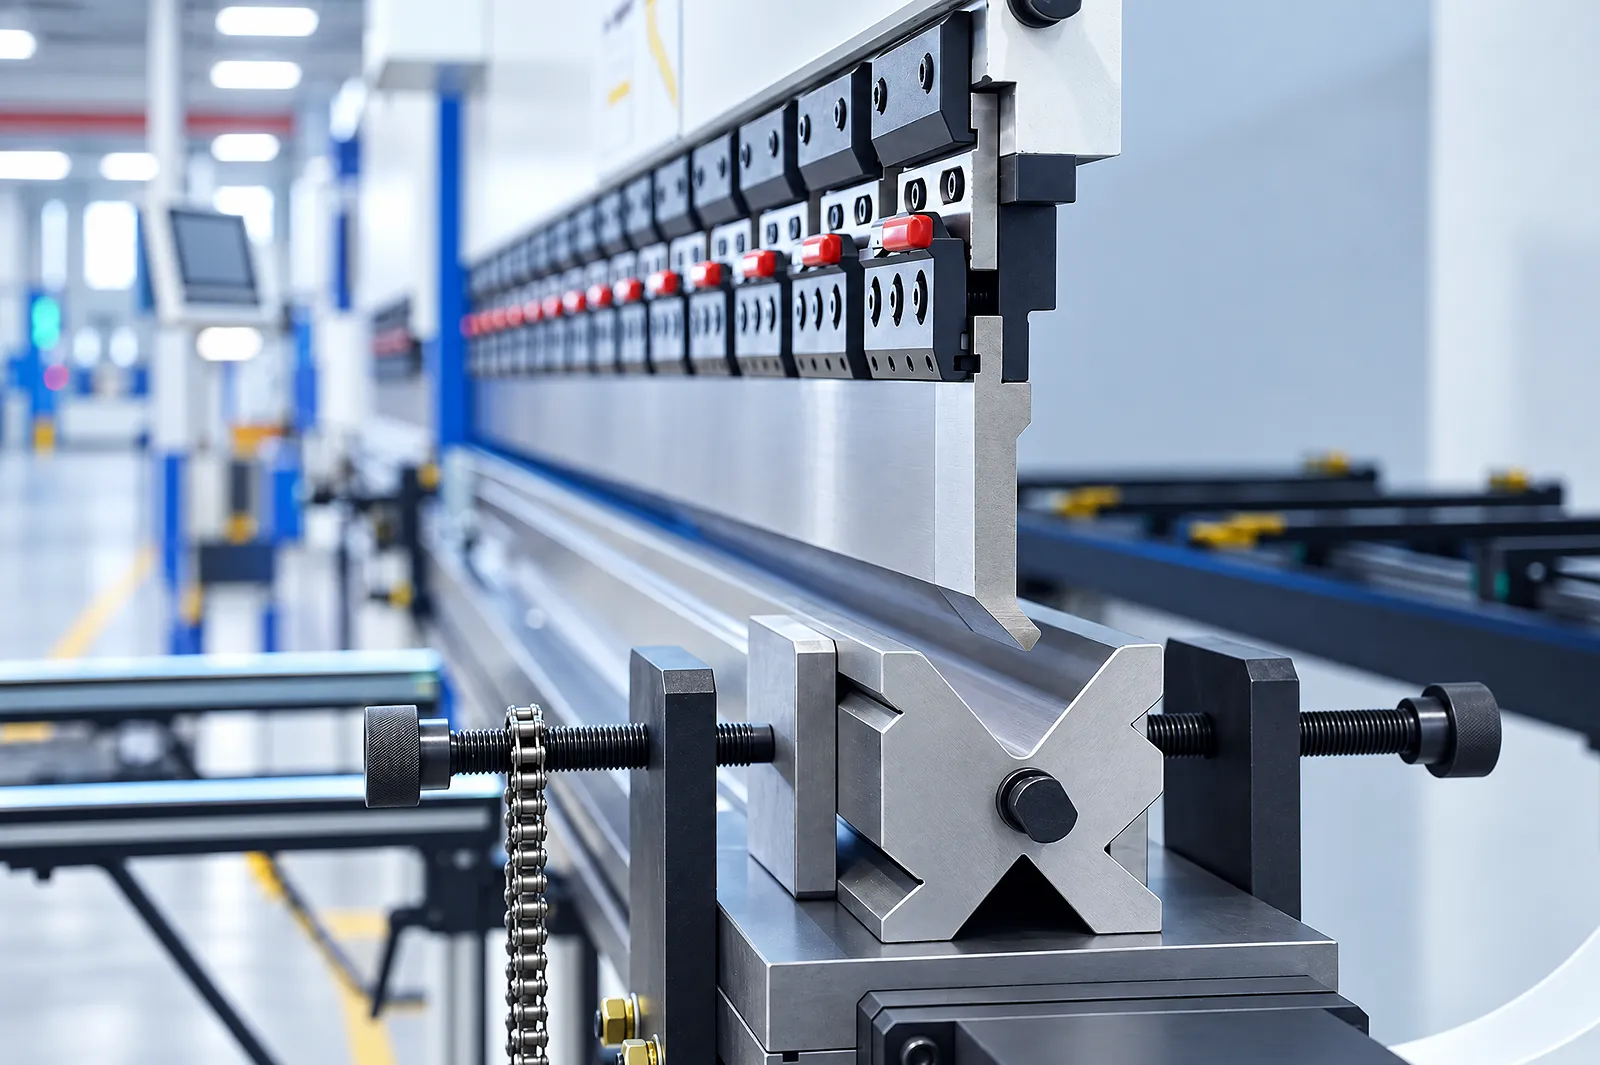
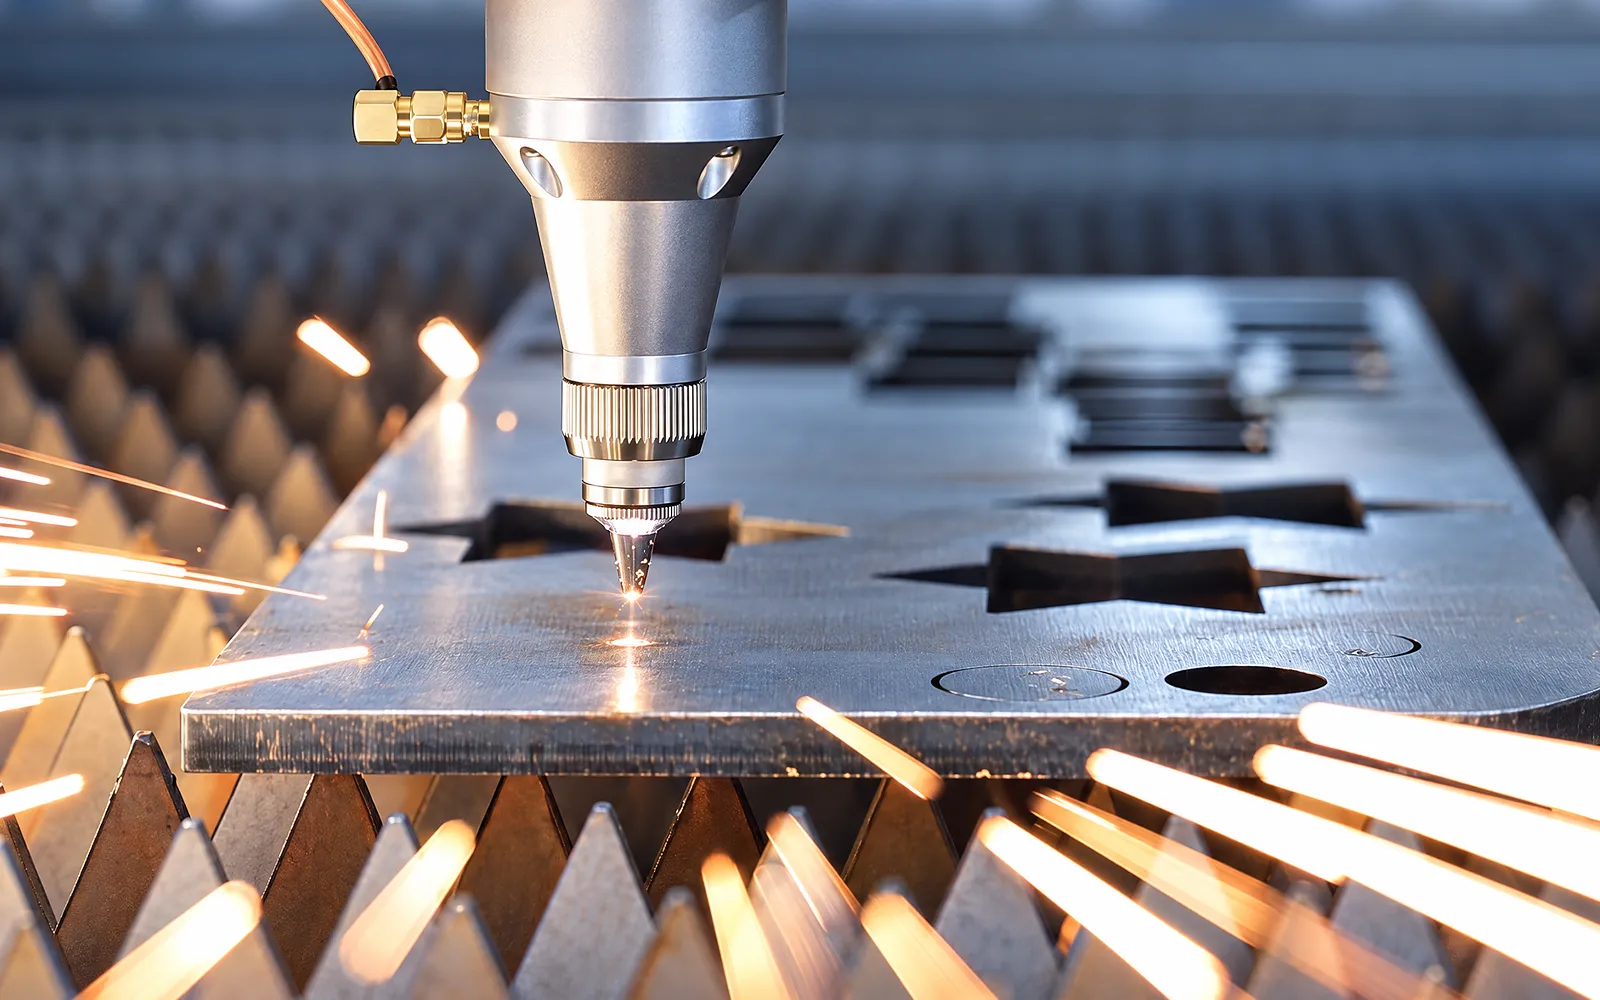
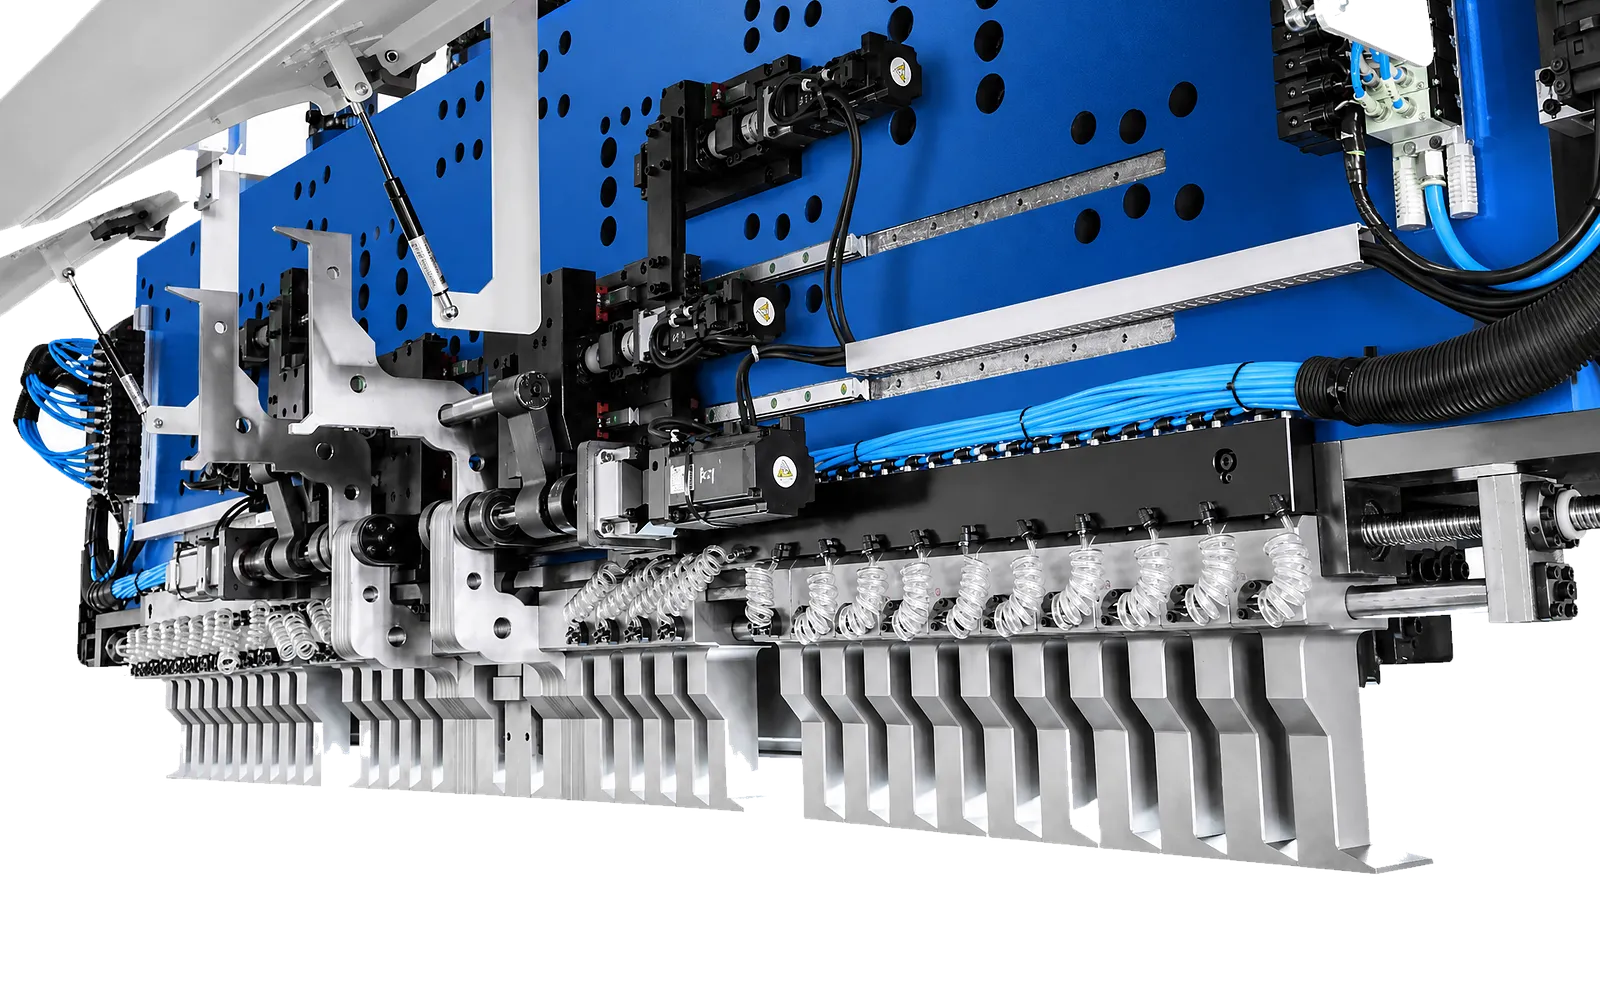
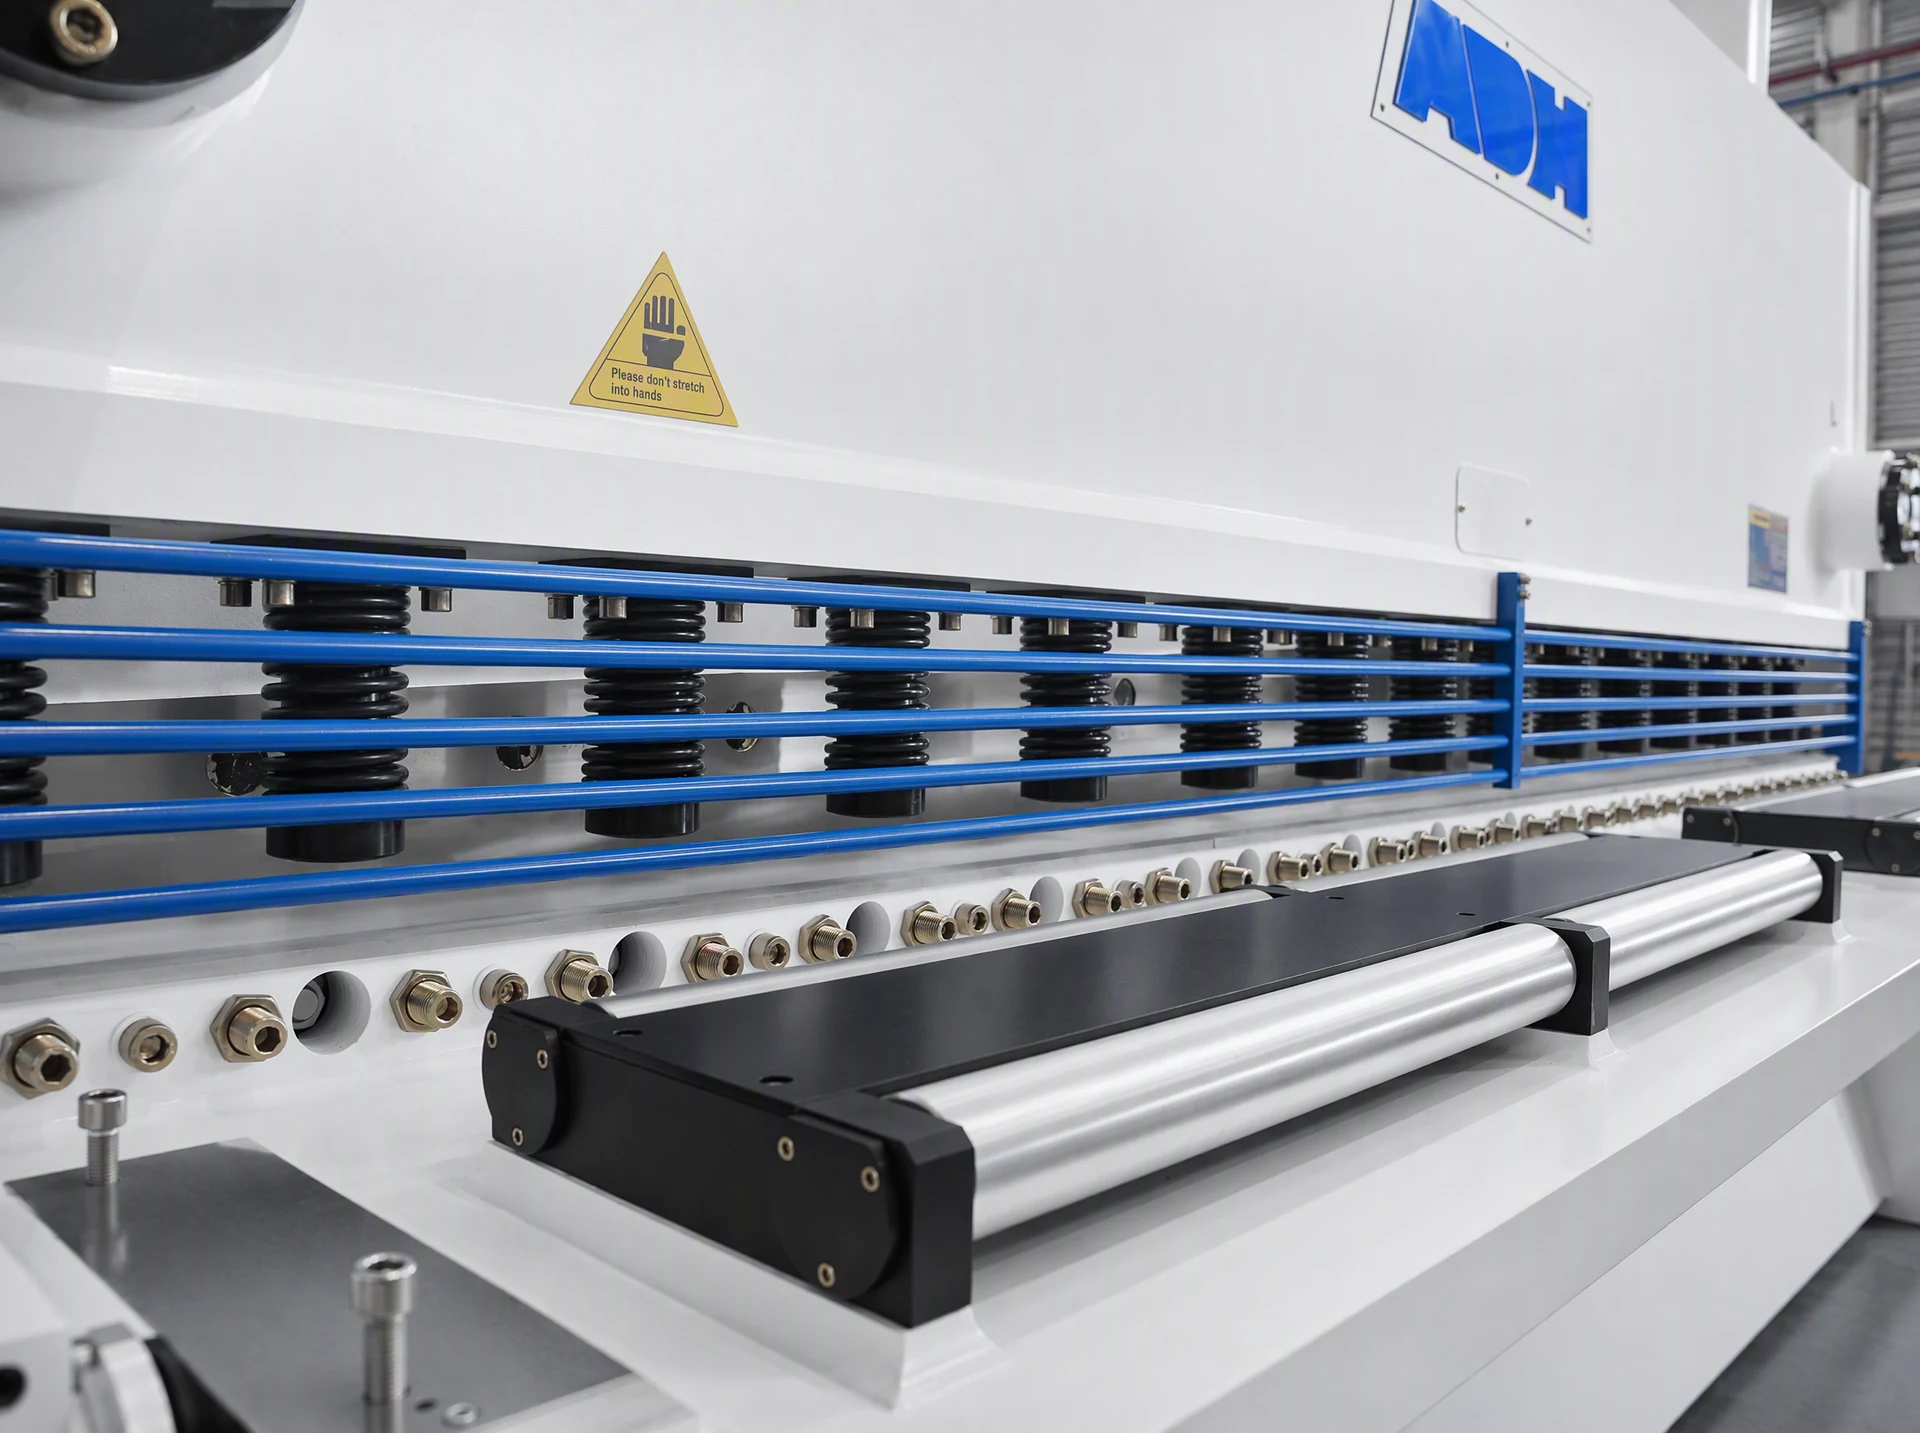
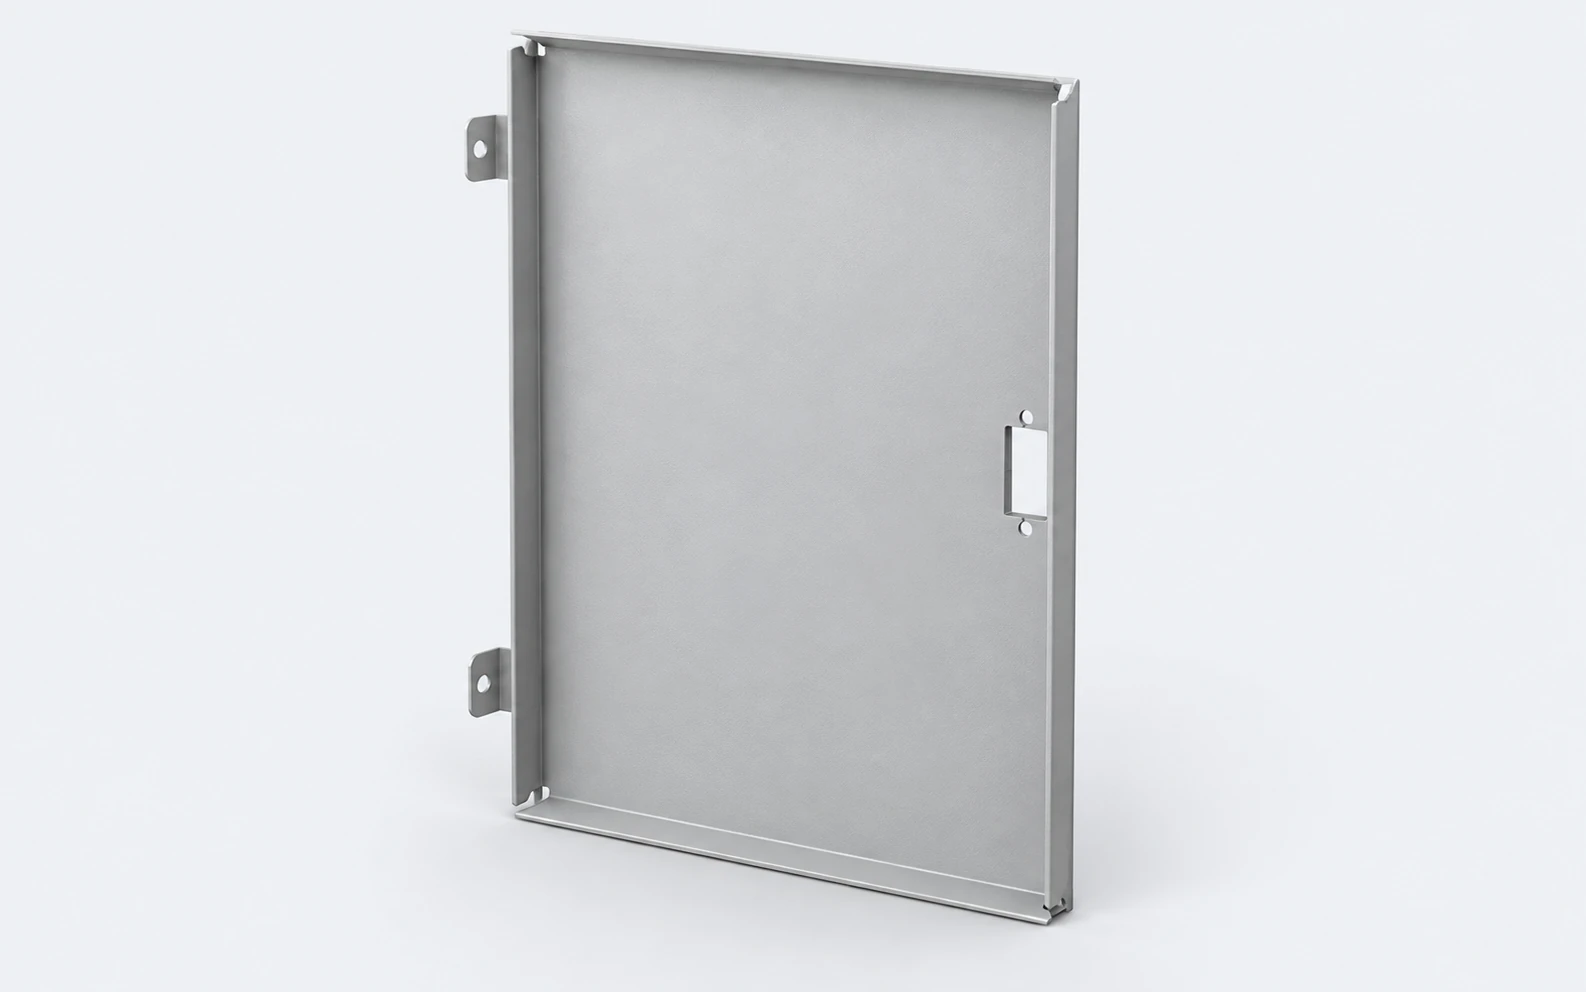
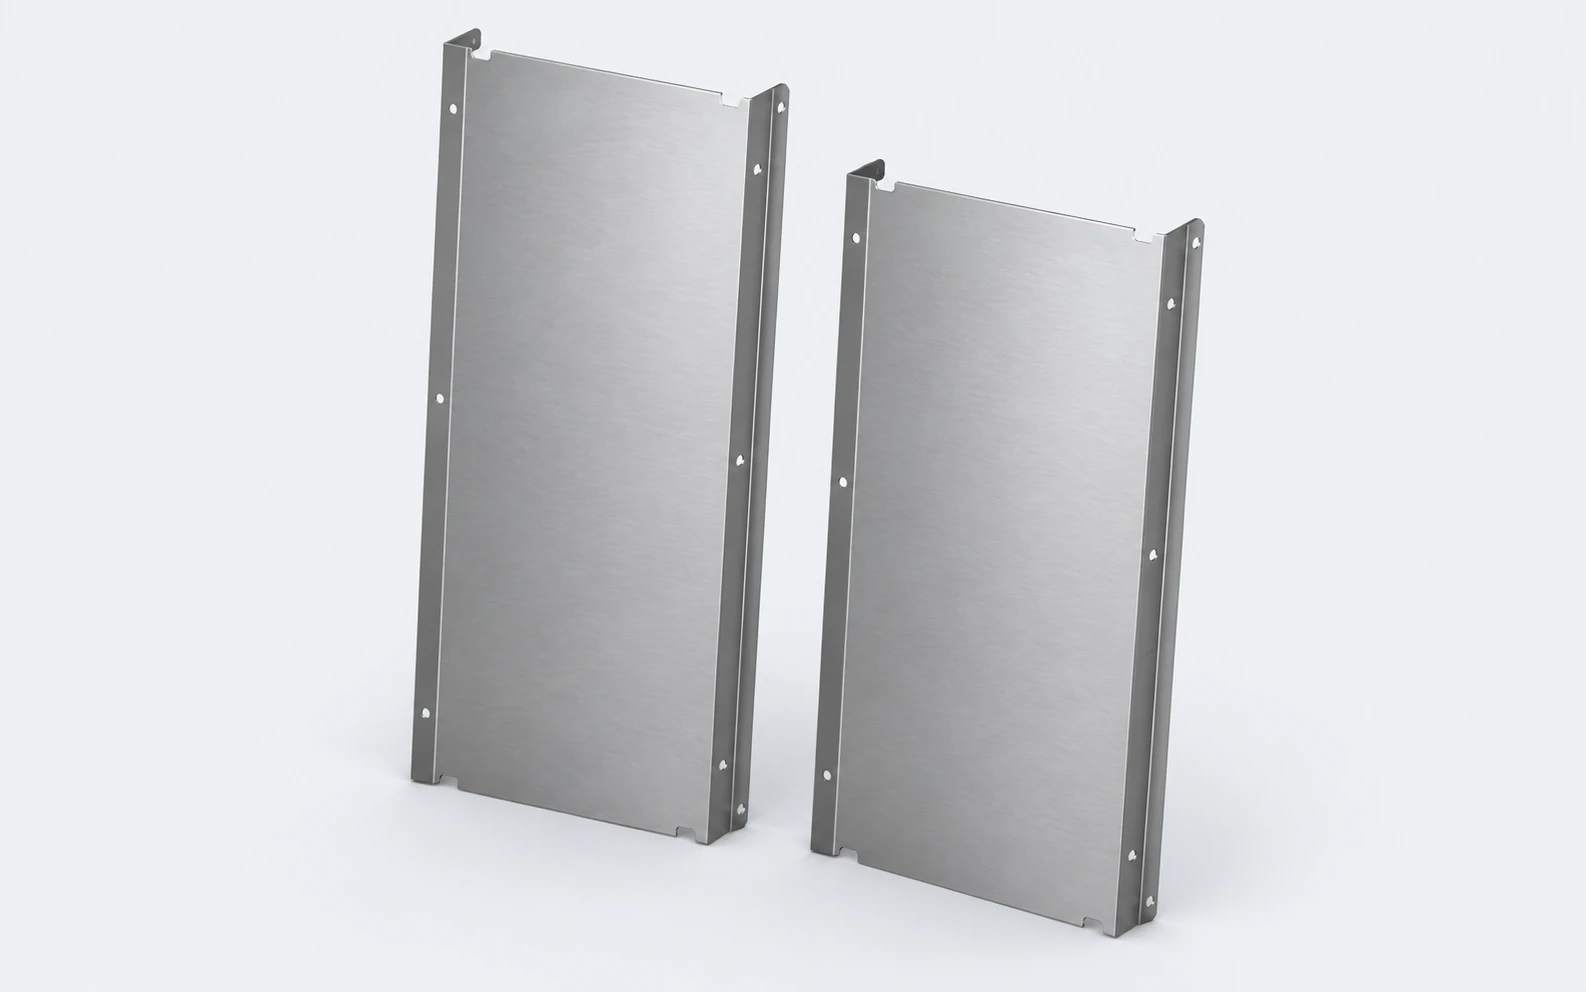
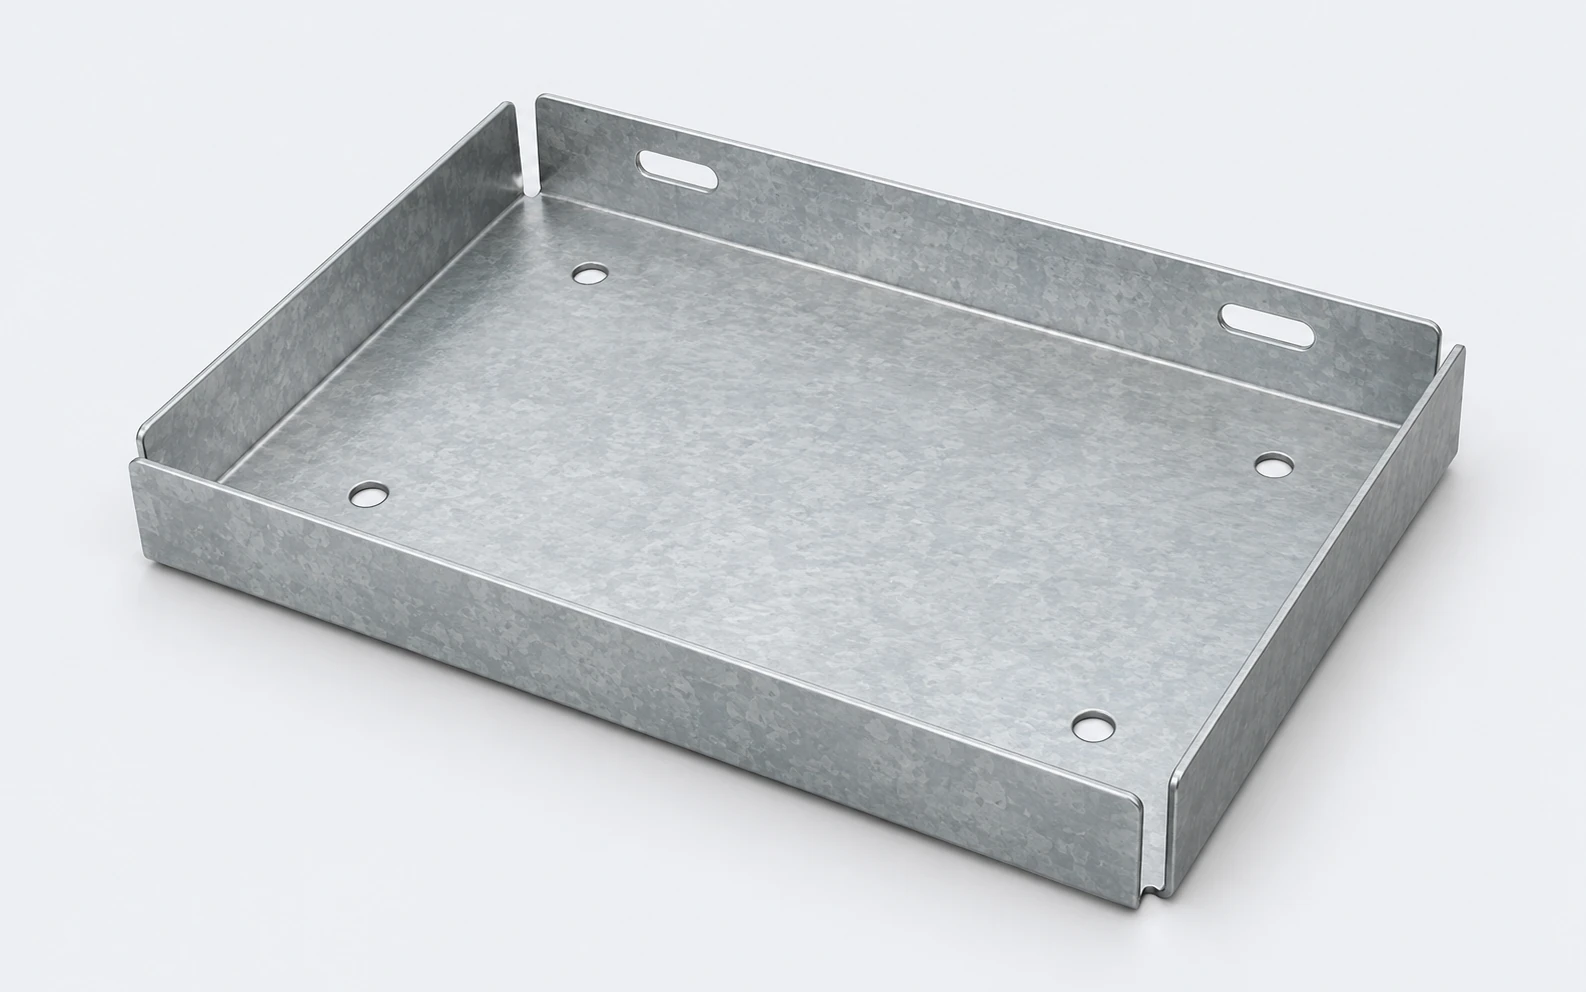
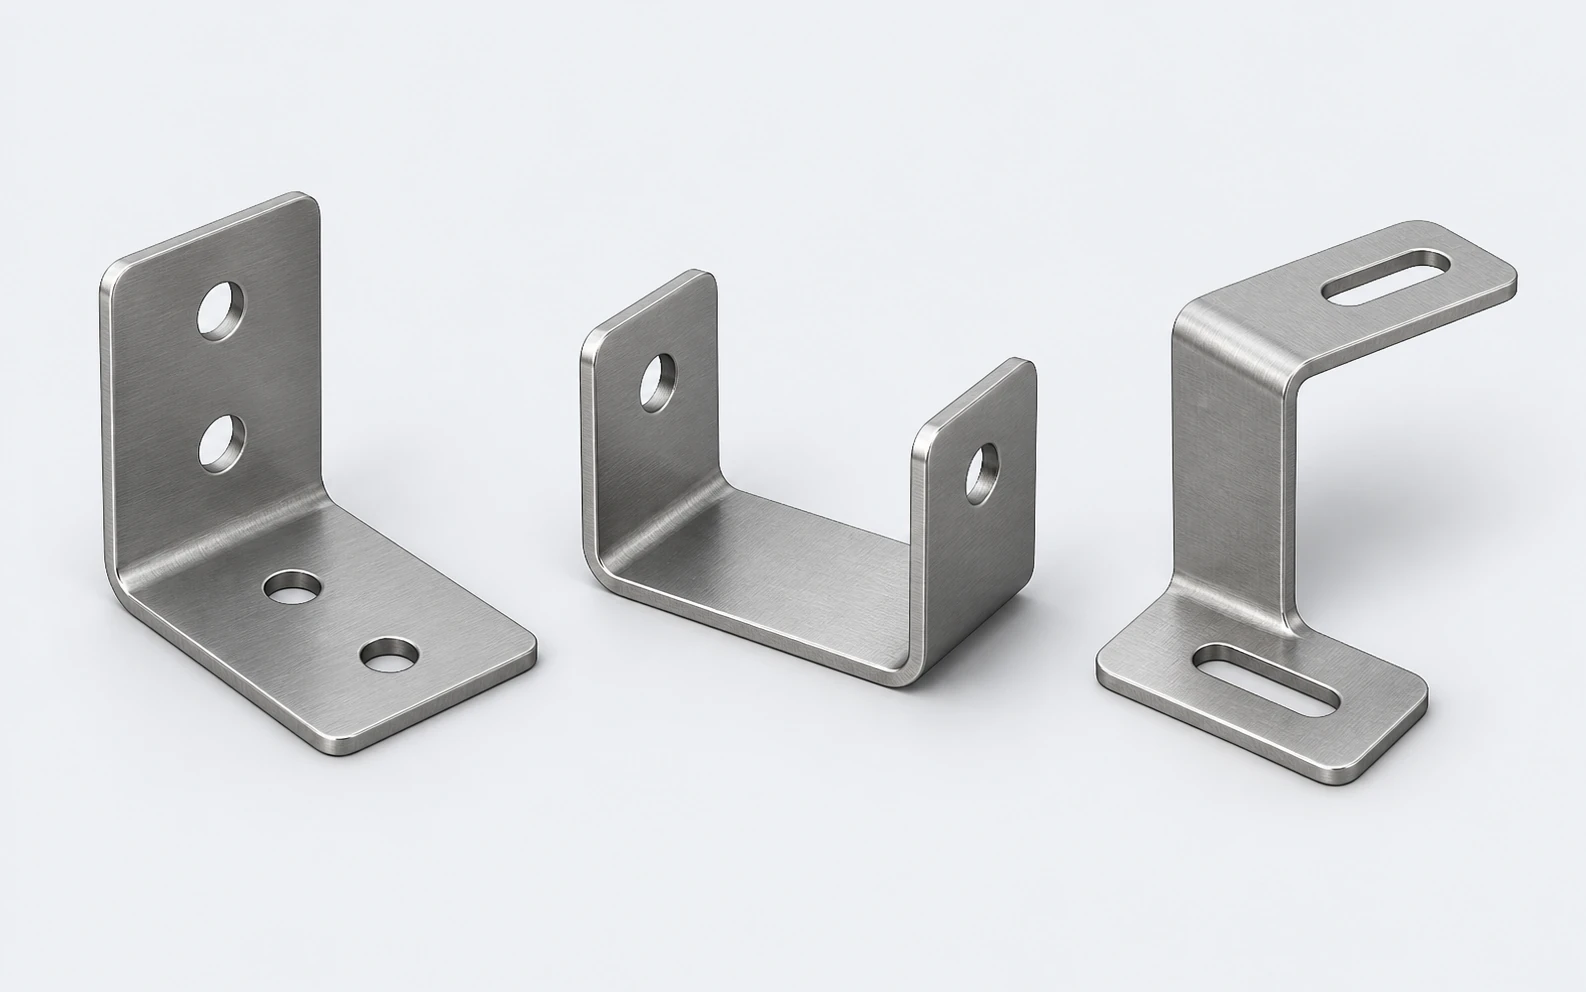
Selection example / Electrical enclosures
Use a door, a tray and a bracket from the same assembly to build a shortlist. This example illustrates a selection method; it is not a verified customer project.
04 / Use the right reference
Use each tool for the question it answers. Record its assumptions alongside the result.
Estimate air-bending force from material, thickness, bend length and die opening. The result does not select a machine or prove tool clearance.
Open bending force calculatorEstimate hourly electricity, entered gas and consumable costs. Add material, labor, setup, maintenance and ownership costs separately.
Open laser cost calculatorEstimate weight from material density and dimensions to start a handling discussion. Check the actual part and equipment load limits.
Open sheet weight calculator05 / Compare proposals
Use the same drawings, batch pattern and quality targets for every proposal. Include regular work and difficult exceptions.
Fit
Agree a representative sample and check the entire sequence: forming or cutting, handling and removal. Record dimensional, angle, edge and surface requirements.
Workflow
Include programming, setup, tool changes, loading, processing and unloading. Compare output over your normal job mix and shifts.
Ownership
List machine, tooling, software, utilities, installation, training and service. Add labor, maintenance and ownership costs to process-cost estimates.
06 / Prepare your brief
01
Send a finished drawing or sketch, dimensions and the feature that is difficult today. Add a flat pattern when available.
02
Give the grade, usual thicknesses and maximum thickness. Identify visible surfaces, protective film and required finish.
03
Describe parts per batch, jobs per shift, changeovers and the current bottleneck. Include typical work as well as outliers.
04
Start with country and project timing. Add floor space, loading access and available utilities when known.
Start with your name, email and a short description. Drawings and technical details can follow. ADH will help you shortlist equipment and define the proposal.