
I once removed a £3,000 piston pump from a press brake that had been reduced to scrap in under 200 hours. The operator insisted he had followed every instruction correctly. He consulted the manual, saw “AW46,” and purchased a drum of generic hydraulic oil with that exact label.
He had unknowingly doomed his equipment. To him, AW46 appeared to be a universal specification—a guarantee of compatibility that saved the company forty pounds on supplies. In truth, that low-cost oil tore itself apart the moment the system exceeded 14 MPa, leaving metal surfaces grinding directly together. Those letters on the drum indicate only how thick the oil is at a specific temperature. They reveal nothing about whether the fluid can endure the intense, high-pressure environment inside a modern press brake.
Related: Press Brake Maintenance
The “Standard Oil” Trap: Why Viscosity Ratings Are Misleading
The shortcut that cuts pump lifespan in half yet seems “good enough” to many operators
Piston pumps in industrial press brakes are designed to last around 20,000 hours under optimal conditions. Yet they frequently fail after 10,000, 5,000, or even 500 hours. The cause nearly always leads back to procurement. A drum of generic AW46 costs far less than a premium formulation, and when it’s poured in, the machine seems to work properly—the rams move, the pressure builds, the metal bends. It appears “good enough.” For shops that want every stroke to stay within spec year after year, pairing quality hydraulic fluid with equipment engineered for precise load balance—such as the Tandem Press Brake from ADH Machine Tool—helps maintain efficiency and extend pump life under continuous high-pressure cycles.
But the gradual loss of viscosity is a hidden destroyer. As the hydraulic system warms throughout a shift, cheap oil thins beyond its usable range. The protective fluid film separating moving metal surfaces disappears. There’s no grinding noise or visible smoke from the reservoir—only microscopic metal contact that slowly erodes internal bearings. Operators often feel justified in their economical choice until the pump eventually locks up and halts production entirely.
What “Standard Hydraulic Oil” really signifies—and the crucial additives it omits

Field data indicates that over 85% of bearing failures stem from contamination and thermal stress, not merely the oil’s viscosity. Generic AW46 contributes to these failures by eliminating the fluid’s chemical protection. The “AW46” label simply denotes an Anti-Wear fluid with an ISO viscosity grade of 46—meaning it flows at 46 centistokes at 40°C. That describes a physical property, not a chemical formulation.
Generic containers meet this minimal physical specification but exclude the costly chemical additive packages. They lack strong zinc-based anti-wear agents, advanced anti-foam ingredients, and the heat stabilizers needed to tolerate high temperatures. When a press brake drives oil past 60°C, a premium fluid depends on these chemical stabilizers to maintain the protective film. A generic oil, by contrast, simply overheats—it breaks down, oxidizes quickly, and allows water and debris to damage the system.
Think of viscosity like a shoe size. Size 10 describes a dimension, yet a size 10 canvas sneaker and a size 10 steel‑toed leather boot perform very differently if a steel beam hits your foot. AW46 only defines the “size” of the oil; the additive package is the steel toe.
Why meeting the basic datasheet criteria still leads to pump destruction under high pressure
A typical oil datasheet prominently presents its 46 cSt viscosity grade and a basic flash point, readily meeting procurement requirements. Since press brakes are built to run on AW46-class fluids, the documentation appears flawless. Yet those paper specifications conceal the mechanical realities occurring inside the machine.
Modern press brakes work under extreme conditions. They drive fluid through proportional valves under severe loads, often exceeding 14 MPa of pressure. In such environments, low-grade oil experiences shear. Lacking advanced anti-foam additives, it releases entrained air, and the tiny bubbles travel into high-pressure zones within pumps and valves, where they collapse violently against metal surfaces.
This microscopic cavitation pits the hardened steel with countless tiny craters. A £40 cost saving on a drum of oil can directly result in a £15,000 bill to replace pumps and valves. The datasheet guaranteed compatibility but concealed the fluid’s complete inability to endure the intense pressure cycles of a working press brake.
The 14 MPa Threshold: Where Basic Lubrication Physically Fails
At only 5 MPa—about 725 PSI—just 0.5% of undissolved air in standard ISO VG 46 mineral oil can reduce the fluid’s bulk modulus by half. Well before a press brake reaches its operational tonnage, that small fraction of air transforms a rigid hydraulic column into a compressible, unstable system. Volume decreases of up to 1% occur at these comparatively low pressures, creating lag and instability in the ram cylinders. If a basic fluid already struggles to retain its structural integrity at 5 MPa, pushing it beyond 14 MPa (2,000 PSI) virtually ensures mechanical failure.
In a press brake, hydraulic oil serves as more than a transmission medium—it functions as a liquid structural bearing. It must physically support the machine’s full bending load while confined between rapidly moving steel surfaces. Using a generic oil in such conditions is like fitting a plastic bearing in a steel rolling mill. Once the system surpasses 14 MPa, the immense mechanical force tears the normal oil film apart, leaving bare metal grinding against bare metal.
The Invisible Conflict Between System Pressure, Temperature, and Oil Film Strength
During press brake cycles, the hydraulic fluid is trapped in a harsh interaction of pressure and heat. As system pressure surges to form heavy-gauge steel, the fluid is forced through minute clearances inside the pump. This friction produces localized heat spikes, briefly driving oil temperatures far above the 60°C average in the reservoir. The heat thins the oil, reducing its dynamic viscosity precisely when maximum film thickness is essential to prevent the pump’s brass slipper pads from seizing against the steel swashplate.
Fluid dynamics show that as pressure rises, the oil film becomes the sole barrier against catastrophic friction. At 14 MPa, the mechanical shear forces actively attempt to tear apart the oil’s hydrocarbon chains. Premium fluids employ complex polymer viscosity modifiers that act like microscopic springs, resisting shear and preserving the separation between moving parts. Standard fluids lack these resilient polymers, and their molecular structures flatten under stress.
Once the film gives way, the pump’s internals behave like a high-speed milling machine.
Anti-Wear (AW) vs. Extreme Pressure (EP): Building the Boundary Film for Vane and Piston Pumps
Piston and vane pumps withstand these harsh conditions through chemical protection rather than simply relying on fluid viscosity. When extreme pressure squeezes out the physical oil film, the system depends entirely on a secondary safeguard—the boundary film. At this point, the difference between basic Anti-Wear (AW) and Extreme Pressure (EP) additives becomes critical to the survival of your equipment.
Typical AW additives, usually zinc dialkyldithiophosphate (ZDDP), are activated by heat. As metal surfaces contact and generate friction, ZDDP decomposes and deposits a sacrificial layer of zinc–phosphorus glass onto the steel. This layer erodes instead of the metal beneath it. However, standard AW formulations have a limit: under severe shock loads during heavy bending operations, the pressure can pierce the thin zinc coating.
This is where EP additives come into play. Containing sulfur and phosphorus compounds, EP agents chemically react with the metal under much higher temperatures and pressures to form a tougher, more resilient protective layer. A generic drum marked “AW46” may include a minimal amount of zinc to qualify legally as an anti-wear oil, yet it will lack the robust EP chemistry needed to endure repeated 14 MPa shock loads.
Cavitation vs. Wear: Two distinct failure mechanisms demanding different additive solutions
Many operators mistakenly believe that high pressure itself causes cavitation. In fact, the phenomenon is more complex: intense pressure compresses trapped air bubbles until they dissolve entirely into the hydraulic fluid. The real damage begins when this pressurized fluid flows through a proportional valve and suddenly releases into the low‑pressure return line. That rapid transition can be controlled far more precisely with advanced hydraulic circuits—such as those engineered in ADH Machine Tool’s CNC Press Brake—where optimized flow dynamics and rigid structural design minimize cavitation risk while sustaining consistent bending accuracy.
The abrupt, violent pressure drop makes the dissolved air rapidly expand back into bubbles. Moving at high velocity, these bubbles are slammed against the hardened steel of valve spools and pump housings, where they immediately implode. Each implosion produces microscopic fluid jets striking the metal at supersonic speed, creating tiny pits in the surface. This is cavitation—it appears as though the metal was corroded, but the damage is purely mechanical.
Preventing wear requires strong boundary-film chemistry such as zinc and sulfur compounds. Preventing cavitation demands advanced anti-foam agents and air-release additives to stop bubble formation within the reservoir. Generic oils fail on both counts, leaving machinery vulnerable to two entirely separate forms of self-destruction.
Decoding the alphabet system: Why HM and HG fluids are essential for high-pressure shear
The letters printed on an oil drum represent a legal classification, not mere marketing. The International Organization for Standardization (ISO) specifies an alphabetic code that defines the precise chemical protection a fluid must provide. “HL” oil is simply refined mineral oil with rust and oxidation inhibitors—ideal for lightly loaded, low-pressure systems but certain to destroy a press brake pump within weeks.
If a system operates above 14 MPa, an “HM” classification is the minimum standard required. The ‘M’ certifies a proper concentration of anti-wear additives to form the necessary boundary film. Yet high-end press brakes, especially those requiring extreme precision, often use “HG” oils. The ‘G’ denotes the presence of specialized friction modifiers that eliminate stick–slip chatter in heavily loaded cylinders, ensuring smooth ram motion under full tonnage.
Buying a generic “AW46” fluid circumvents this entire classification system, leaving you unaware of the actual chemical composition of the oil. You could easily end up pouring an HL fluid into an HG-rated machine. The pump will eventually destroy itself, and the damage will not stay confined to its housing. The microscopic steel fragments produced by that failure will remain suspended in the fluid, now circulating toward the precision proportional valves where they will cause further damage.
The Chemistry of Precision: Protecting Proportional Valves and Seals
A proportional valve spool operates within a fluid film clearance of about three microns—a fraction compared to a human hair’s thickness of seventy microns. When the generic AW46 in your system breaks down at the pump, producing microscopic steel debris, these hardened particles do not settle harmlessly in the reservoir. They are propelled directly into that three‑micron clearance at high speed. The fluid ceases to act as a lubricant and instead becomes a liquid abrasive. As the spool moves to stabilize the ram, the embedded shrapnel scratches the hardened steel of the valve body. You will not hear it happening; you will simply notice the press brake can no longer hold bend angles within half a degree, leading to a $12,000 servo valve replacement.

Shear stability: What happens to molecular chains during a 200-ton bend?
Imagine a coiled spring. Premium hydraulic fluids contain polymer viscosity modifiers that function like such springs at the molecular scale. When the press brake drives down with 200 tons of force, the oil is forced through tiny valve orifices at 14 MPa. This mechanical shear attempts to tear those polymer chains apart. In a high-grade fluid, the polymers stretch as they pass through the constriction and then recover their shape, absorbing the stress while preserving the fluid’s viscosity.
Generic fluids lack that flexibility. Their molecular chains are rigid, and under the same 200‑ton load, the mechanical stress literally breaks those hydrocarbon chains. This results in irreversible viscosity loss. Oil that began the shift at ISO 46 may exit the valve block behaving like an ISO 32. The thinner fluid can no longer maintain the load-bearing film needed to keep the spool separated from the valve body. Metal-to-metal contact occurs, generating another wave of fine debris that accelerates wear.
Zinc-Free or High-Zinc? Aligning oil chemistry with your servo valve metallurgy
Typical anti-wear additives rely on zinc dialkyldithiophosphate (ZDDP). Although 700 parts per million of zinc offers excellent boundary protection for hardened steel pump vanes, it creates a serious issue when used in systems with older or highly specialized servo valves. Many of these precision valves contain internal components made from bronze, brass, or copper.
Zinc is chemically aggressive toward yellow metals at elevated temperatures. As the fluid heats during heavy bending operations, zinc additives begin to extract copper from the bronze bearing surfaces, causing the valve to deteriorate internally. This is why adding a high‑zinc AW46 without verifying the valve block’s metallurgy can be disastrous. Zinc‑free, or ashless, formulations were created to address this issue. They employ alternative sulfur‑phosphorus chemistry to protect steel components without damaging bronze. Knowing the exact metals present inside your valves is essential before selecting a fluid chemistry for your system.
The mixing multiplier: How chemical incompatibility during a top‑off can destroy an entire additive package
Maintenance technicians often refill a low reservoir with whichever AW46 drum is nearest to the machine, assuming that matching viscosity means compatibility. This assumption frequently leads to total hydraulic system failure.
Additive packages are delicately balanced chemical mixtures. When a zinc-based AW46 is blended with an ashless, zinc-free AW46, their conflicting chemistries react with each other instead of with the metal surfaces. The additives leave suspension completely, creating a viscous, gel-like sludge that settles at the tank’s bottom and blocks the suction strainers. Even worse, the fluid loses both its anti-wear protection and shear stability. The sight glass might still show “full,” but chemically, the oil is no longer functional.
A five-minute top-off can nullify the same chemical defenses that keep proportional valves operating. Yet even with flawless chemical management, the pump begins to fail the moment shop temperatures fluctuate. When a standard fluid experiences a complete viscosity index collapse, no amount of intact additive chemistry can prevent cold-start cavitation that destroys the pump early in the morning, or thermal thinning that erodes bend precision by midafternoon.
The Viscosity Index Paradox: Surviving Cold Starts and High-Cycle Heat
Most equipment makers specify a strict upper limit of 860 centistokes (cSt) for hydraulic pump startup viscosity under load. Leaving a generic AW46 fluid overnight in a shop that drops to 5°C lets that oil behave more like chilled molasses than a liquid, easily exceeding the 860 cSt threshold. Temperature variation alters the oil’s flow resistance before the machine is turned on. The viscosity paradox is that the same thickness protecting the pump at operating temperature becomes its destroyer at startup. Hydraulic oil serves as a liquid structural bearing; if it cannot adjust to the ambient temperature, it fractures under the press brake’s tonnage before the first part is produced.
Cold start viscosity spikes: The critical period when pump cavitation is most likely
Imagine a piston pump’s suction inlet trying to draw fluid at seven on a January morning. Standard AW46 oil is rated for 40°C and flows smoothly at that temperature. At 5°C, however, its flow resistance increases dramatically. As the pump rotates mechanically to create suction, the thickened fluid cannot move quickly enough through the strainer to fill the chamber, generating localized zones of extremely low pressure inside the pump.
This pressure drop becomes so intense that dissolved air in the oil vaporizes, creating microscopic bubbles. Within milliseconds, as the pump transitions into the high-pressure discharge stage, these bubbles are hit with about 14 MPa and collapse violently. This is cavitation. Each implosion sends a tiny shockwave that chips a microscopic crater into the pump’s hardened steel housing. You might notice a brief rattling sound, like marbles in a blender, that fades as the equipment warms up. Operators often dismiss this as the machine “waking up,” while in fact they’re hearing the pump gradually destroy itself, one tiny fragment at a time.
Thermal thinning: How high-cycle heat accumulation undermines bend consistency
Eight hours later, the condition reverses entirely. A press brake performing continuous, high-frequency bending builds up substantial internal friction, driving the reservoir temperature beyond 60°C. Conventional mineral-based AW46 lacks the molecular resilience to retain structure under that heat. The oil thins, dropping from its specified 46 cSt toward the viscosity of water.
A proportional valve depends on the oil’s viscosity to seal the minute clearances between the spool and the valve body. Once the fluid becomes thinner than its operating tolerance, it starts leaking internally past these seals. Although the pump still moves the same oil volume, pressure seeps through the gaps instead of being converted into mechanical force at the cylinders. The ram begins to drift. A bend that was precisely on target at nine in the morning comes out two degrees shallow by three in the afternoon. Operators usually suspect the controller or tooling, wasting hours adjusting offsets, when the real issue is a thermally degraded fluid unable to sustain the load.
For fabricators facing hydraulic instability or heat‑related drift, connecting directly with ADH Machine Tool’s engineering support can clarify whether an alternative fluid formulation or system tuning is needed. Reach out through ADH Machine Tool’s contact page to discuss technical evaluation or implementation options with their specialists.
ISO VG Grade vs. Viscosity Index: Why HVLP fluid becomes essential when ambient temperatures drop below 10°C
A typical AW46 oil has a Viscosity Index (VI) of roughly 95. The VI is a dimensionless indicator of how strongly an oil’s viscosity changes with temperature—the higher the value, the more stable the oil. When shop temperatures fall under 10°C, a VI of 95 becomes problematic because the fluid thickens so much that cold-start pump starvation is inevitable.
Switching to an HVLP grade (High Viscosity Index, normally above 140) is not optional for unheated environments—it is a mechanical requirement. High-end “All Weather” blends employ shear-stable polymer additives to raise the VI to around 157. These polymers behave like thermal springs: contracting in cold conditions to keep the oil flowing freely and below the 860 cSt startup ceiling, and expanding as the fluid warms to limit thinning. If your facility cannot maintain a steady, climate-controlled 20°C, using a standard AW46 in the reservoir directly risks shortening your pump’s life.
Continuous high-heat operations: What synthetics deliver that mineral oils cannot maintain
Certain production demands leave no room for thermal recovery. When a machine runs continuously over multiple shifts, applying high loads with minimal idle time, its hydraulic circuit remains under constant heat stress. Even extensively refined mineral oils eventually fail through thermal oxidation, depositing their additives as dark, tacky varnish on valve spools.
Synthetic hydraulic fluids are designed from pure, uniform molecular structures—unlike the inconsistent chain lengths found in refined crude. This uniformity grants exceptional thermal stability. A top-quality synthetic AW46 remains pumpable down to −30°C, but its key strength appears at high temperatures. Because the molecules move past each other with far less internal friction, the pump generates less heat, often improving overall efficiency by about 8%. The synthetic fluid not only withstands the heat but also minimizes its creation. In doing so, lubrication evolves into a direct enhancement of the press brake’s thermodynamic efficiency.
The Decision Framework: Selecting Your Fluid with Precision
It is established that hydraulic fluid functions as a dynamic structural element whose thermal stability governs pump longevity and machine accuracy. The logical next question is how to transition your press brake to these higher-grade fluids. The process begins by discarding the habit of ordering generic stock and instead building a strict specification profile.
Step 1: Check your system pressure and pump design before opening any product catalog
This framework stems directly from the 14 MPa threshold we established; once your gauge exceeds that level, you are no longer merely purchasing oil—you are defining a structural component that determines whether your pump lasts through the week. The figures on your machine’s data plate are the only ones that matter. Check the maximum operating pressure, then identify the pump’s design. Piston pumps in heavy-duty press brakes commonly reach 20,000 operating hours—often surviving a decade of use—but only when supplied with a fluid that maintains the precise mechanical tolerances those pumps require.
A gear pump running at 10 MPa experiences vastly different shear conditions than a variable displacement piston pump striking 28 MPa during a bottoming bend. High-pressure piston designs depend on microscopic fluid films to separate fast-moving brass slippers from steel swashplates. Without knowing your system’s peak pressure, you cannot determine the fluid’s necessary shear strength to prevent metal contact. Consult the manual, verify the gauge, and record the peak pressure.
Step 2: Correlate your shop’s temperature variation with Viscosity Grade and Index requirements
Viscosity has no meaning outside its temperature range. An ISO VG 46 rating only describes oil thickness in a laboratory maintained at precisely 40 °C, which rarely matches shop conditions.
Record your temperature extremes. Does the facility drop to 4 °C on winter weekends? Does the machine run three shifts in August, elevating the reservoir to 65 °C? If this temperature range exceeds 20 degrees, a standard Viscosity Index of 95 will fail at both limits. Specify an HVLP fluid with a VI greater than 140. This higher index enables the polymer chains to expand and contract as needed to sustain the target 46 cSt viscosity, avoiding cold-start cavitation and high-temperature thinning.
Step 3: Match additive classification (HL → HM → HG) to your pressure conditions
Now align the chemistry with the applied force. Hydraulic fluids are categorized by their additive formulations, where the generic “AW” label often causes issues. An HL-rated oil includes rust and oxidation inhibitors suitable for low-pressure equipment such as a log splitter but is disastrous in a press brake.
Once your system surpasses 14 MPa, it operates in extreme-pressure territory. You must choose an HM-class fluid, containing the heavy-duty anti-wear additives necessary to prevent boundary lubrication failure. If the machine includes heavily loaded sliding ways sharing the hydraulic circuit, an HG classification may be required to avoid stick-slip chatter. Match the grade to the load—never use HL oil in an HM environment.
Step 4: Cross-reference OEM approval lists to safeguard warranty and seal integrity
The final checkpoint lies with the manufacturer’s engineering team. OEM approval lists are sometimes dismissed as marketing devices, but they are actually detailed compatibility assessments.
Advanced synthetics and high-load additive systems interact chemically with elastomers. A fluid that fits your pressure and temperature criteria might still cause specific Buna‑N seals to contract or Viton O‑rings to swell and extrude. Consulting the OEM list ensures that the chemistry protecting your pump does not compromise the seals retaining the fluid. Once a formulation satisfies all four steps, you have identified your replacement fluid. The remaining challenge is introducing it into the reservoir without contamination.
Beyond the Pour: Moving toward a Condition‑Based Fluid Strategy
The 10-Micron Misconception: Why brand-new oil from the drum is often the dirtiest part of your system
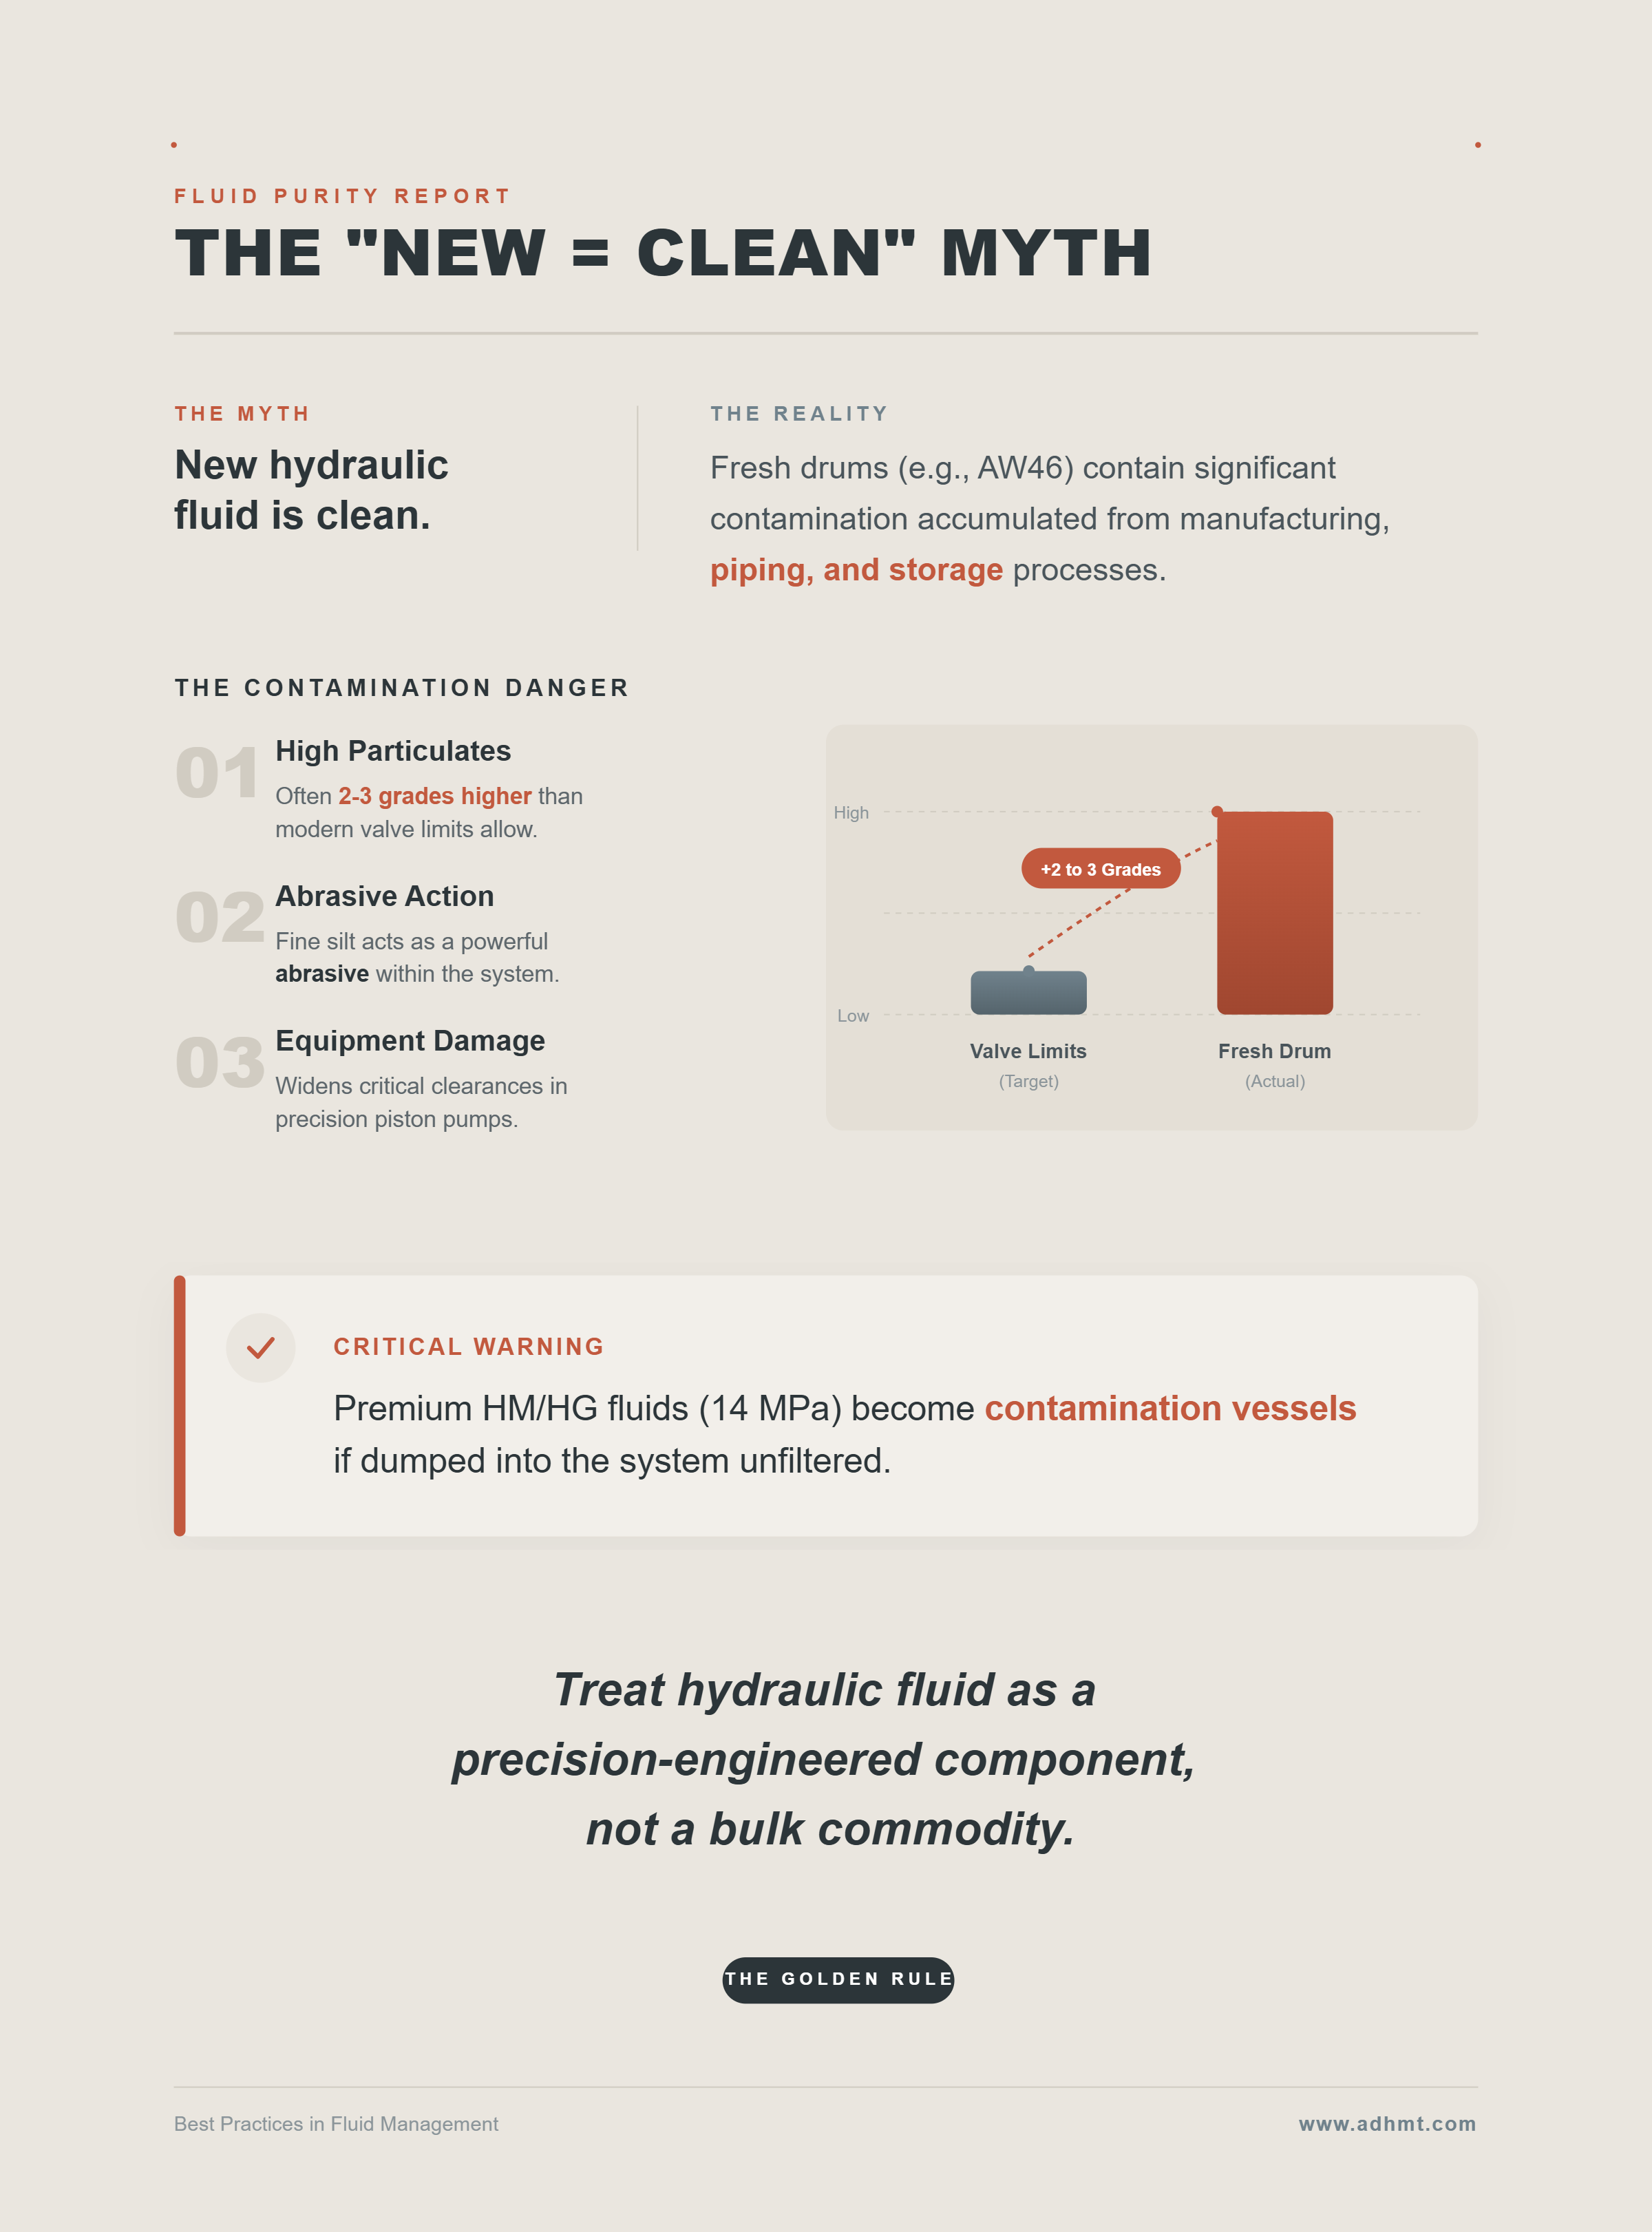
The most dangerous belief in a maintenance shop is that “new” means “clean.” Opening a fresh drum of generic AW46 does not reveal a sterile fluid but one that has moved through industrial piping and been stored in steel containers. These drums frequently have particulate levels two to three grades higher than what modern press brake proportional valves can handle. Pouring that oil directly into a reservoir amounts to self-inflicted damage. The fine silt acts like an abrasive compound, gradually widening the critical clearances inside a piston pump. Even if you choose a high-performance HM or HG fluid designed to withstand 14 MPa, dumping it unfiltered into the tank simply turns an expensive product into a transport vessel for contamination. The guiding principle is straightforward: handle hydraulic fluid as a precision-engineered component, not as a bulk commodity.
Understanding how contamination starts is only half of protecting your equipment. Integrating disciplined cleaning routines ensures that every drop of hydraulic fluid performs as designed. For practical steps on keeping the pumping circuit and reservoir in peak condition, see How to clean and maintain a press brake, donde ADH Machine Tool explica métodos basados en su experiencia de I+D en sistemas CNC para prevención de impurezas y desgaste prematuro.
Pre-filtering and Kidney Loops: The only reliable approach for introducing new fluid to a press brake
Since fluid is a precision component, the only approved method for transferring it from a new drum is through a dedicated filter transfer cart. Oil should never be “poured”; it must be “transfused” through a 3‑micron absolute-rated filter before entering the reservoir, capturing the “new-oil silt” in a disposable element instead of in the bearings of a pump worth thousands. For systems already operating, maintaining a continuous off-line “kidney loop” filtration setup removes wear metals that regular return filters miss. Still, this represents only basic mechanical cleanliness; even the purest oil will fail if its chemistry cannot withstand the pressures generated by a press brake.
Quick Field Checks: Detecting early signs of noise, vibration, or foam that signal a fluid mismatch
Human hearing is often more sensitive than most sensors for spotting a mismatch before major damage occurs. If a high-pitched, metallic “marbles in a blender” noise arises during heavy bending, that is not ordinary machine sound. It is the noise of generic AW46 breaking down under load. The pump attempts to move a fluid without the anti-wear chemistry required to withstand 14 MPa, creating microbubbles that implode with enough force to pit steel surfaces within the pump’s rotating assembly. Increased vibration and cloudy, foaming oil in the sight glass are final warnings. Once foam appears, the inferior oil’s additive system has failed. The ram then rides on air pockets, eliminating precision in bending operations.
Diagnosing “Varnish”: Recognizing when chemical breakdown surpasses mechanical wear
Over time, the heat and shear from exceeding the 14 MPa limit will degrade the oil, producing the hidden enemy of proportional valves: varnish. If a valve spool shows a sticky, gold or tea-colored residue that cannot be wiped off, the fluid has chemically failed. This is the costly conclusion of the “AW46 is AW46” misconception. Adopting a condition-based method means choosing fluids—HM or HG types—formulated for the actual pressures and temperatures of the equipment, rather than purchasing by generic viscosity rating. This creates a concrete operational standard instead of a simple preventive maintenance task. After spending decades removing metal fragments from scorched pumps, I can confirm this: once you stop treating the press brake reservoir like a basic tractor gearbox, the five‑figure repair bills stop as well. The next time you see a low-cost drum of standard AW46, remember the real cost that will show up by Monday morning.
Related Resources and Next Steps
- For teams evaluating practical options here, Large Press Brake is a relevant next step.
- For readers who want detailed materials, brochures is a useful follow-up resource.