Press Brakes · CNC Systems

CNC Press Brakes

CNC bending with independent Y1/Y2 control. Compare WAD and WADE by working range, controller and production needs.

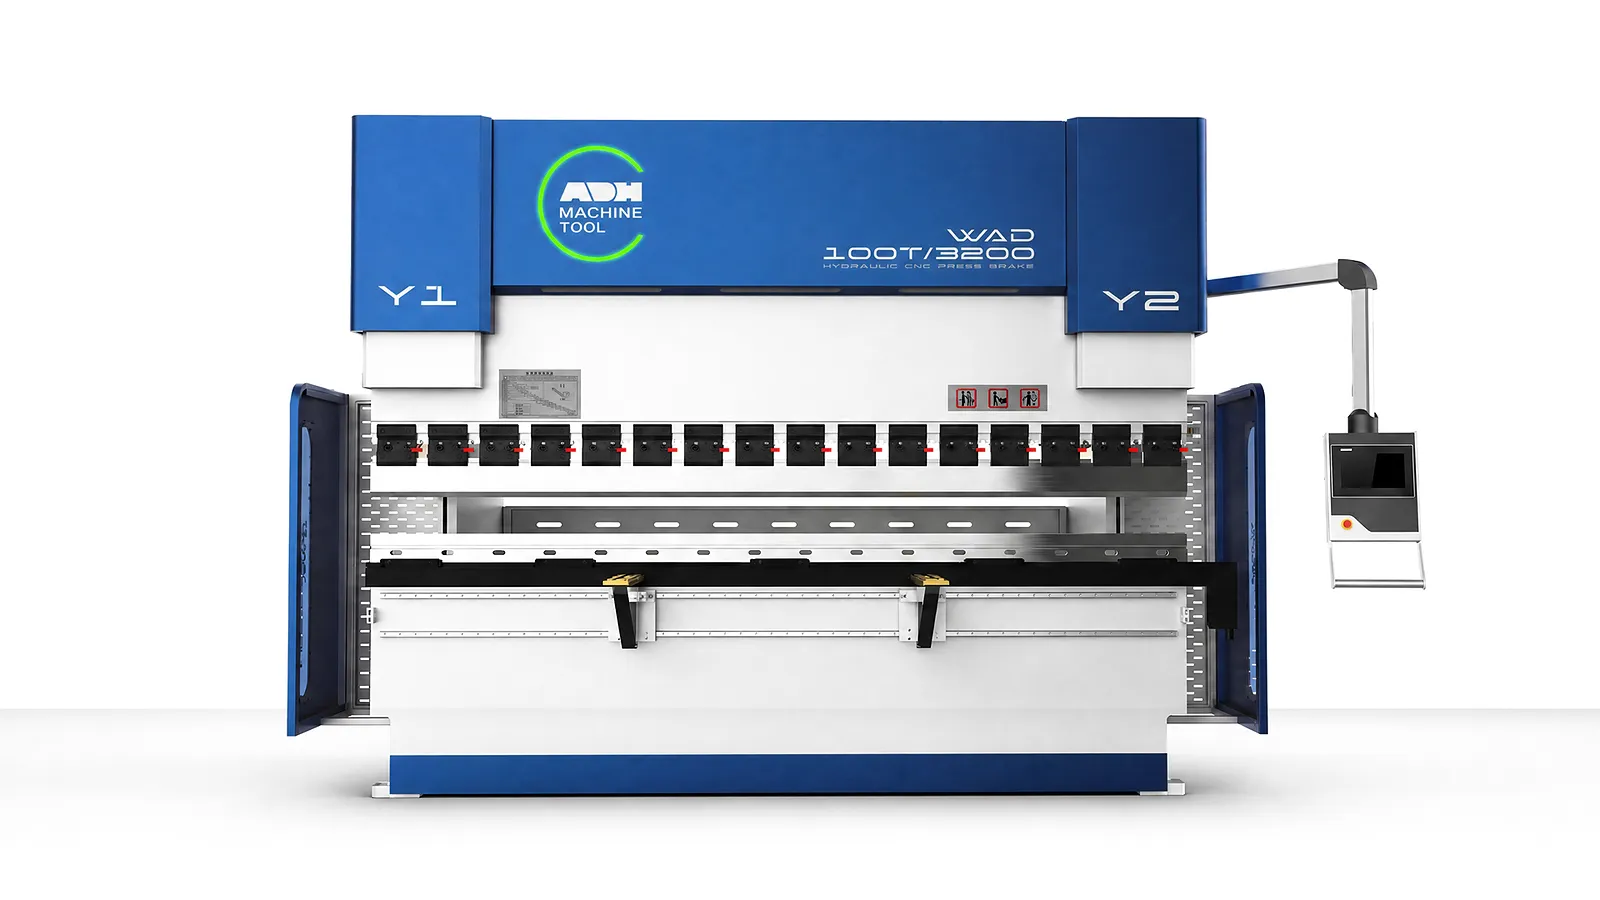
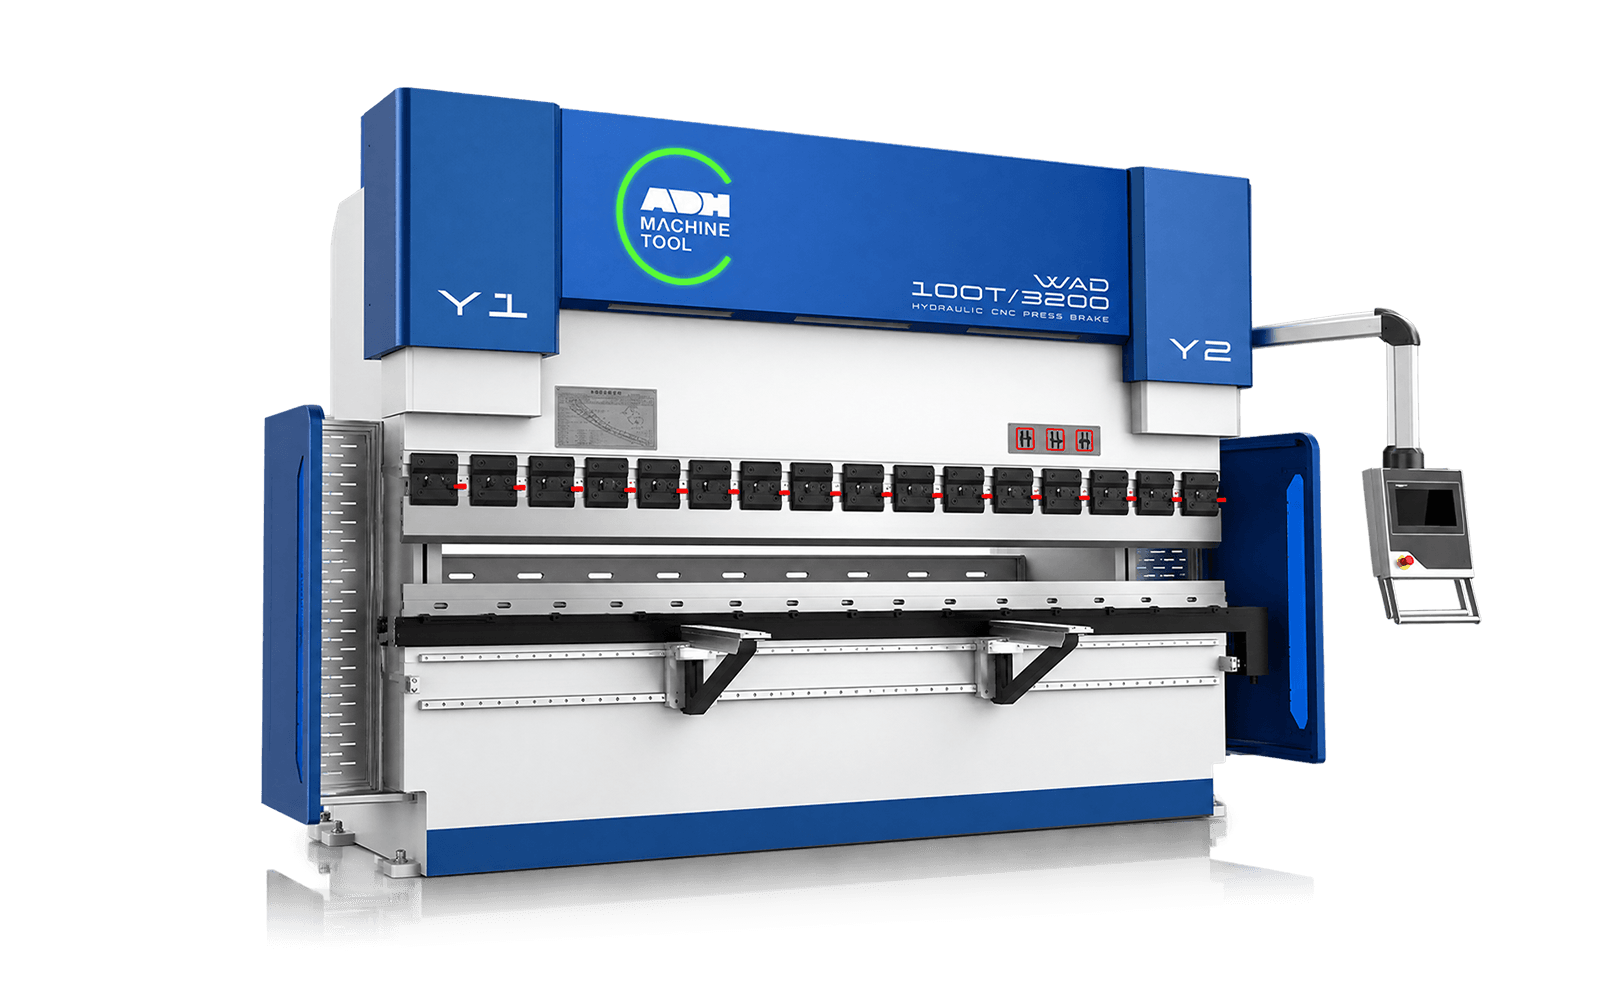
ADH WAD electro-hydraulic servo CNC press brake

Selection comparison

WAD or WADE? Compare the differences

Start with the controller workflow, then choose one model from the matching series table. Both platforms use electro-hydraulic force and independent Y1/Y2 position control.

Compare

WAD

WADE

Published force range

WAD

50T–300T standard models

WADE

50T–300T standard models

Controller options

WAD

Delem DA-53T, DA-58T, DA-66T or DA-69T; ESA S640 optional. Confirm the selected software and interfaces in the quotation.

WADE

ACS930H, ACS930S or ACS990 controller options.

Model information

WAD

Use the WAD table for working length, opening, stroke, motion and electrical data.

WADE

Use the separate WADE table for working length, opening, stroke, motion and electrical data.

A force range covers multiple models. Compare programming, axes, tooling and the exact specification row using the same representative part.

CNC series

Two CNC press brake platforms

Compare the controller choices below, then check the matching model table for capacity and dimensions.

WAD CNC press brake series

WAD Series

WAD Electro-Hydraulic Servo CNC Press Brake

Choose Delem DA-53T, DA-58T, DA-66T or DA-69T, with ESA S640 optional. Specify axes, tooling and safeguarding for the selected WAD model.

Model range

50T-5000T

Controller options

Delem DA series · ESA S640 optional
View WAD Series
WADE CNC press brake series

WADE Series · ACS Controller Family

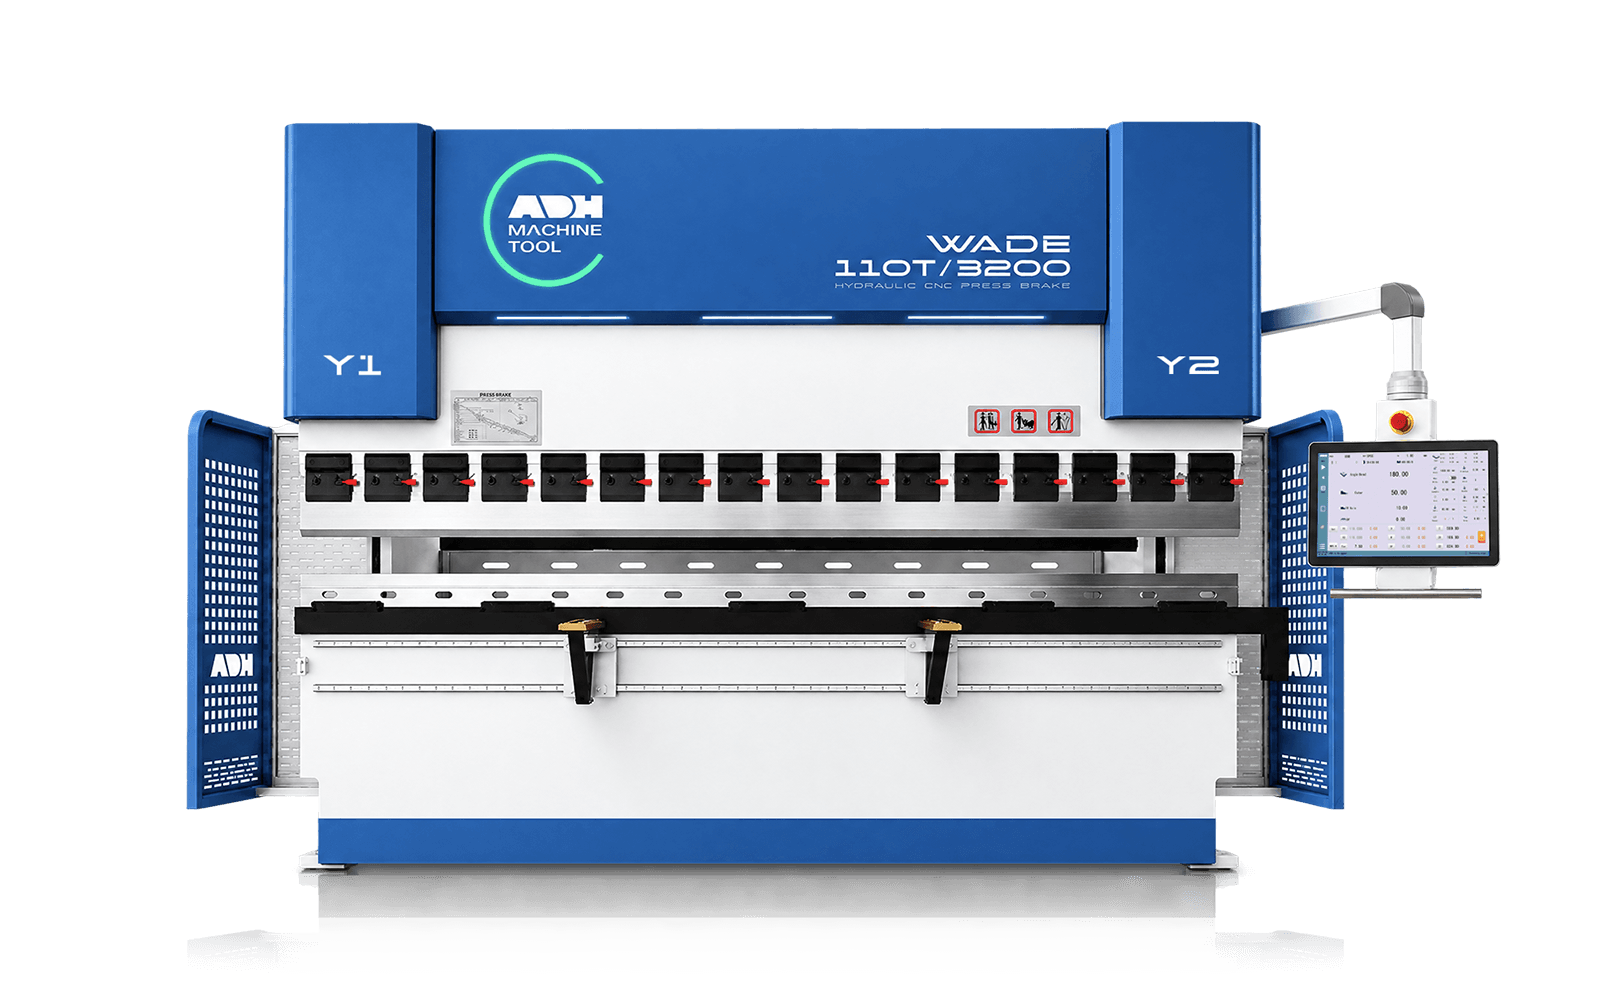
WADE Electro-Hydraulic Servo CNC Press Brake

Choose ACS930H, ACS930S or ACS990 for the selected WADE model. Confirm axes, tooling and electrical equipment in the quotation.

Model range

50T-300T

Controller family

ACS930H / ACS930S / ACS990

View WADE Series

Applications

CNC bending for the way you work

Use the production pattern to compare WAD and WADE. A controller demonstration is most useful when it follows one of your own jobs.

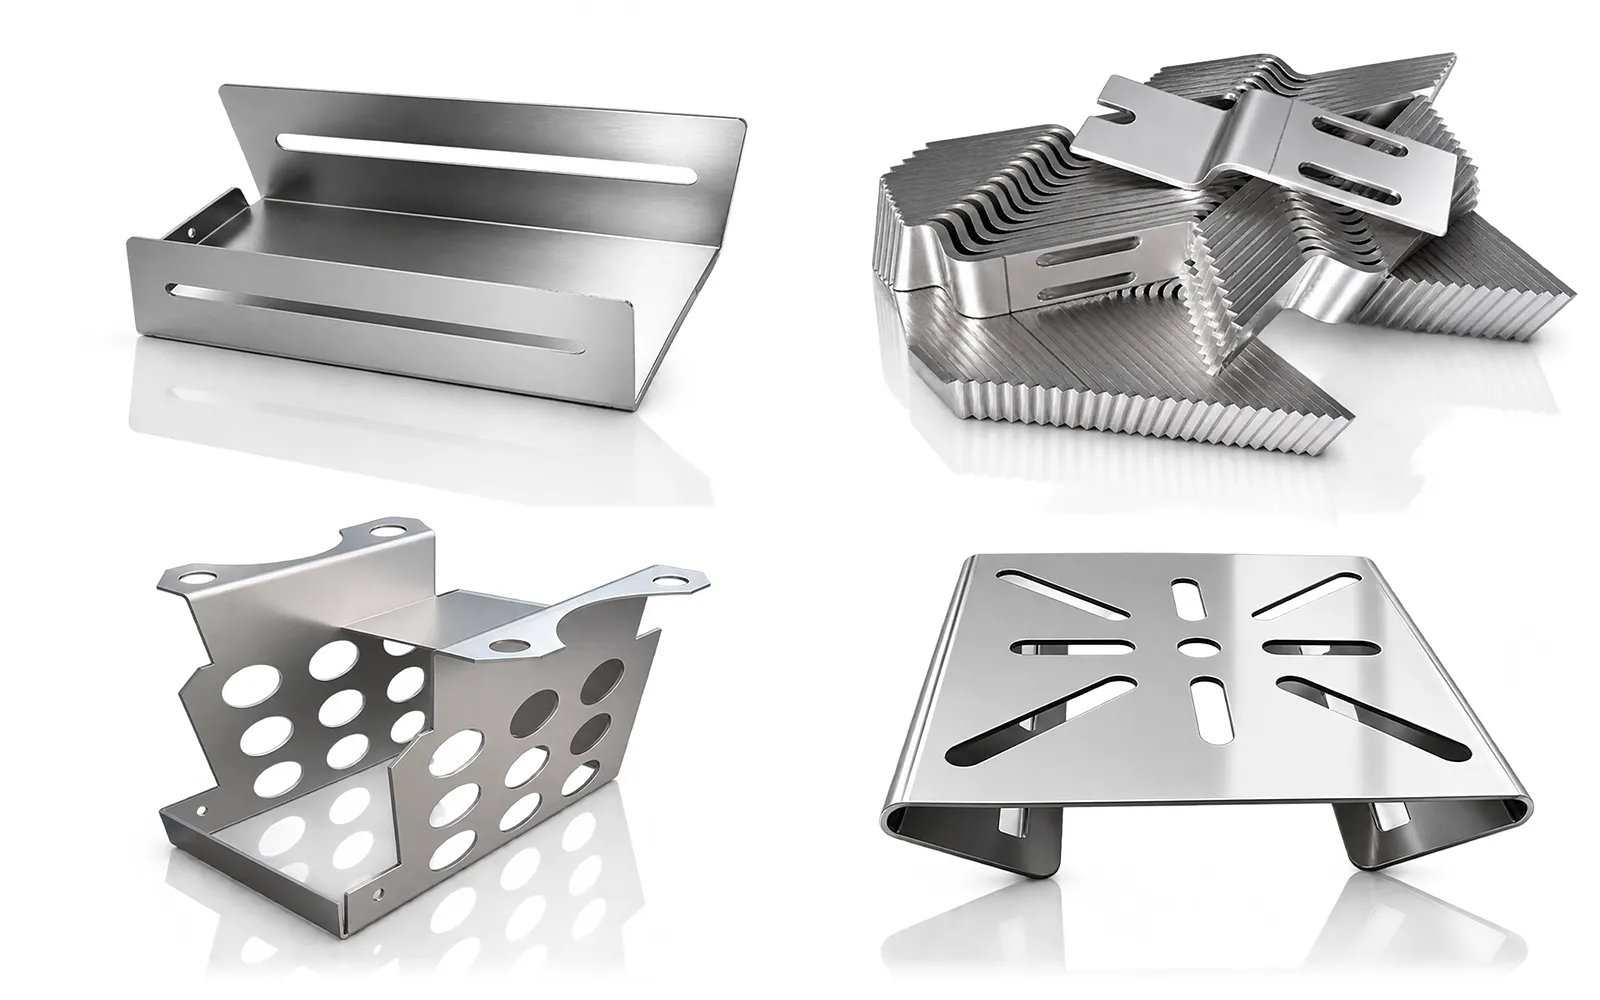
Assorted bent sheet-metal trays and brackets

01

Frequent job changes

For varied small batches, follow the whole changeover: drawing input, bend program, tool setup, first part and program recall.

Ask to see: the workflow your operators will repeat.

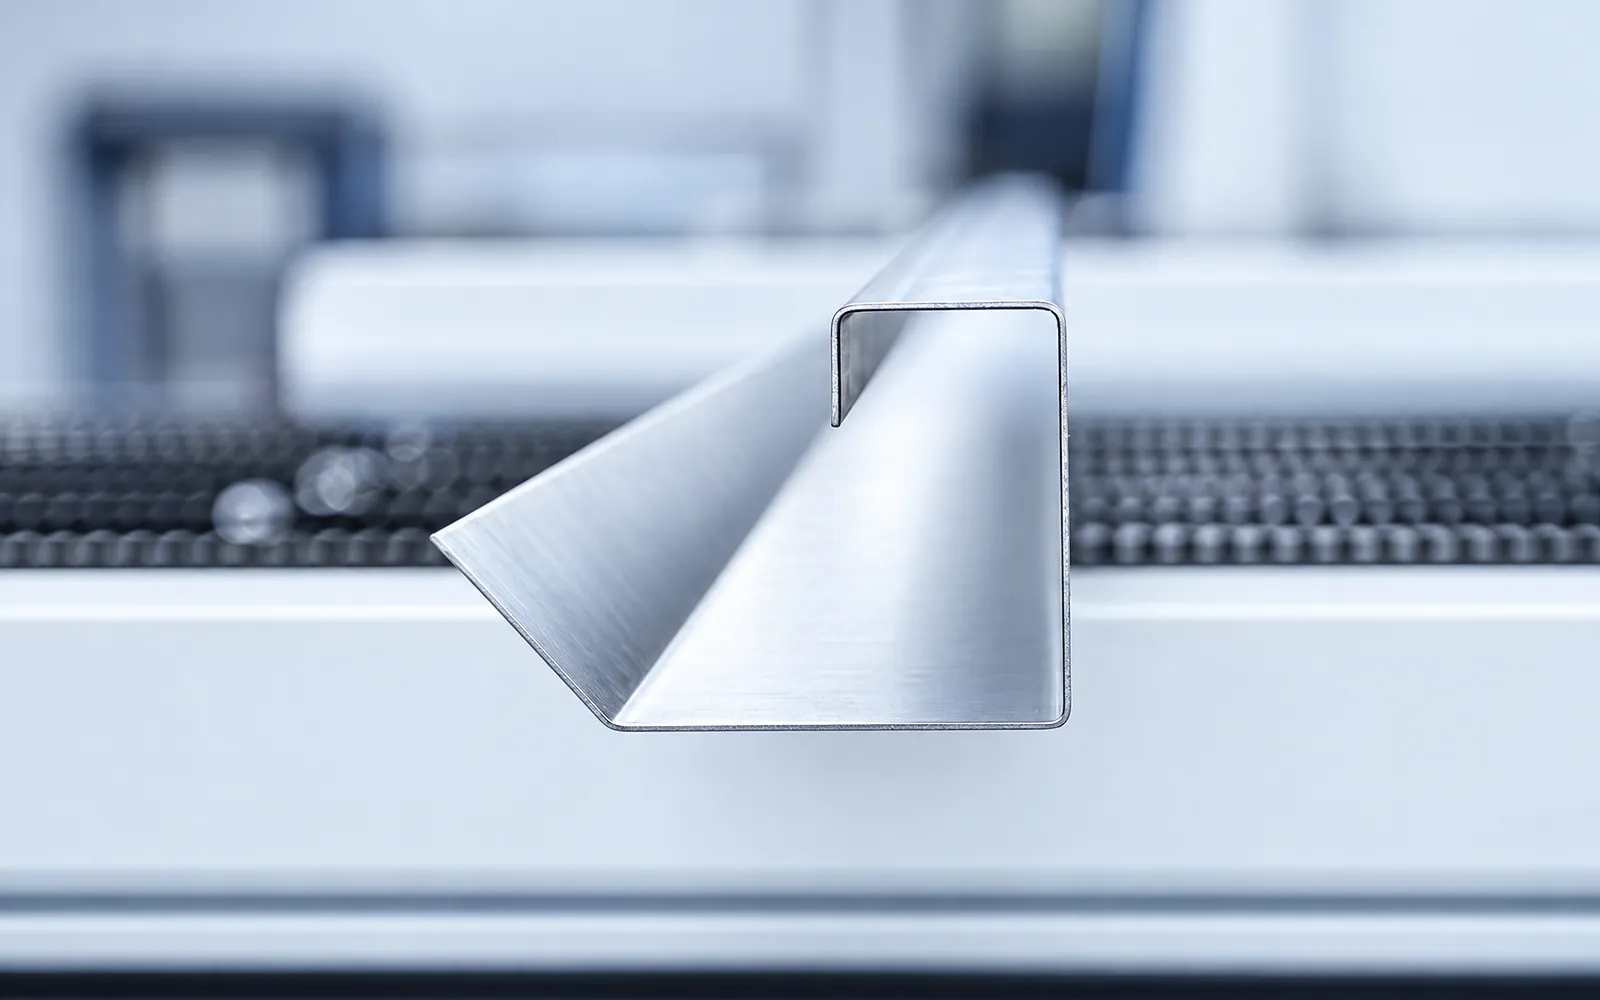
Sheet-metal profile with several bends and return flanges

02

Multi-bend components

Parts with several reference edges may need more than one backgauge movement. Review how each bend is positioned and how the part is turned.

Ask to see: the complete bend sequence and reference points.

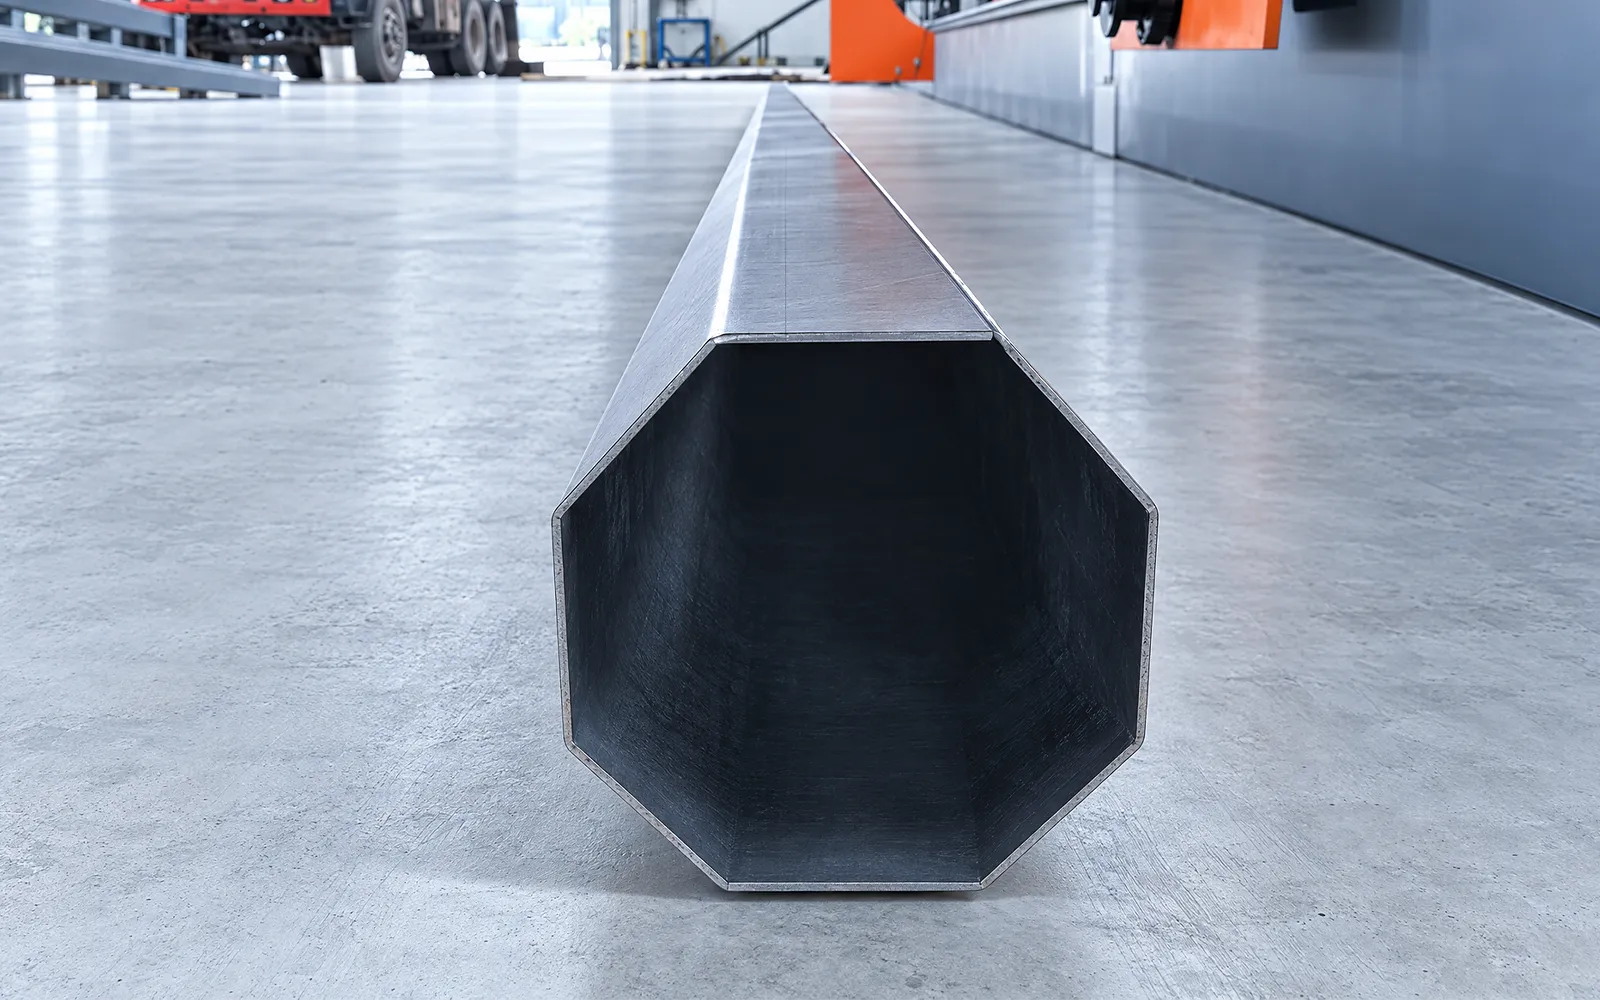
Long metal section with an octagonal cross-section

03

Long production parts

Long bends make support, crowning and inspection across the working length important. Include the real sheet size in the discussion.

Ask to see: a suitable part-support and angle-check method.

Application inputs

Choose around your parts

The workpiece determines force, working length, tooling, axes and handling. Controller and electrical requirements then guide the choice between WAD and WADE.

01

Material and force

Provide grade, strength, thickness, bend length, flange geometry, radius and the force/tooling calculation.

02

Program and tooling

Share drawings, angle targets, bend sequence, die opening, tool interface, clamping and crowning requirements.

03

Control and handling

Define controller workflow, axes, program transfer, supports, follower or robot interfaces and operator tasks.

04

Site and acceptance

Provide power supply, installation limits, destination standards, safeguarding requirements and the sample-part measurement plan.

How the bending system works

The systems behind each bend

Closed-loop ram control, backgauge positioning, tooling and safeguarding work together through every bend. The selected model and quotation define the supplied components.

Y1/Y2 synchronization

Independent cylinder control and direct position feedback correct ram position through the programmed stroke. Hydraulic and motion values follow the selected model.

Backgauge and axes

Define datums, X/R travel, additional axes, stop fingers, support and automation interfaces from the part.

Tooling and crowning

Match punch, die, opening, line load, clamp type and compensation method to the bend plan.

Safety and acceptance

Specify optical protection, controls, guarding, destination requirements and the signed sample test.

Buying guide

Compare the controller package in practical terms

WAD and WADE have separate model and controller packages. Choose by the functions required for your process and team.

01

Programming tasks

Check drawing input, program editing, simulation, tool-library handling and language needs using the selected controller.

02

Included hardware

List the supplied axes, backgauge arrangement, tooling, clamping and measurement options in each quotation.

03

Training and transfer

Confirm how programs move between office and machine, which software licences are included and what operator training covers.

Selection path

Plan your CNC press brake project

Submit the same part, tooling, handling and acceptance information for both series so the comparison reflects the actual production job.

01

Submit the production brief

Part drawings, materials, bend plan, output, handling and site requirements.

02

Compare WAD and WADE

Compare series-specific controllers, axes, tooling and exclusions, then select one model from the matching published table.

03

Approve the acceptance plan

Agree the sample part, measurement method, safety requirements and responsibilities in the technical agreement.

FAQs

CNC press brake selection questions

Compare the practical controller, axis and tooling package for WAD and WADE.

How do WAD and WADE differ?

WAD offers Delem controllers with ESA S640 optional; WADE offers ACS controllers. Compare dimensions, electrical data and working limits in each series’ own specification table.

Review WAD Review WADE
How many backgauge axes do I need?

Start with the reference edges and positioning moves needed for each bend. Extra axes are useful when they reduce manual repositioning or help reach the required references. Ask for a demonstration of the complete part sequence and confirm which axes the proposed controller and machine include.

Review backgauge options
Does a more advanced controller guarantee better bend accuracy?

Bend accuracy also depends on material, tooling, machine condition, feedback, crowning and setup. Compare sample-part results alongside the controller’s programming workflow.

Can I prepare programs away from the machine?

Offline programming is available when the selected software and controller package support it. Confirm the licence, file formats, tool library, program-transfer method and operator training. Test the workflow from an office file to a usable machine program before relying on it in production.

Explore offline programming
Are crowning, angle measurement and quick clamps included?

Inclusion varies by series and configuration. Ask the quotation to list crowning, angle measurement, clamps and optional upgrades separately.

How should I compare production speed?

Compare the complete part cycle with the same material, tooling, operator tasks and batch pattern. Published approach, working and return speeds describe individual movements. Programming, tool changes, positioning, part turning and unloading also contribute to the output you can achieve.

Explore applications in your industry

See equipment options for the parts your industry produces.

Project enquiry

Discuss your project

Tell us what you want to make or improve. Technical details and drawings can follow.

  • Material, thickness and part size
  • Drawings and production volume
  • Location and project timing

Contact ADH

Start a machine enquiry

Name, email and a short description are enough to begin.

Contact Form