
Why “Top 10” Lists Let You Down (And How to Choose the Right Machine Instead)
Chances are you’ve spent the past week combing through comparison tables that tell you everything about a machine’s theoretical maximums—and almost nothing about whether it can actually earn its keep. “Top 10” lists fall short because they judge industrial manufacturing equipment the way people shop for consumer electronics, ranking models by features-per-dollar instead of reliability-per-shift.
A workshop doesn’t need a generic “winner” picked by a tech blogger; it needs a machine that fits real-world constraints: budget timing, daily throughput, and required finish quality. Rather than chasing a ranking, build a requirements matrix that maps your production needs—especially materials and volume—to the capabilities that truly matter.
For instance, if your top priority is high-precision metal cutting and long-term production stability, consider industrial-grade options like the Single Table Fiber Laser Cutting Machine, built for streamlined throughput in professional environments.
The Spec-Sheet Trap: Why Wattage Is the Least Useful Metric When You’re in a Rush
Common Mistakes When Prioritizing Workshop Equipment
- Prioritizing peak wattage over process stability is one of the most expensive mistakes workshop owners make.
- High wattage doesn’t matter if the machine suffers from gantry misalignment or demands heavy post-processing.
- Wattage mainly affects maximum cutting thickness, not profitability.
- Pay attention to hidden “downtime drivers,” not just tube power specs.
- Key downtime drivers include nozzle and lens cleanliness, servo maintenance intervals, and consistent cooling airflow.
- If you care about revenue, the metrics that matter most are acceleration and kerf-width consistency.
- A well-tuned 60W machine can outperform a poorly calibrated 100W model.
- An unstable machine wastes both material and time, making extra wattage a net negative.
If consistent uptime and precision are critical to your operation, reviewing professional systems such as the Dual-use Fiber Laser Cutting Machine With Cover can help maintain uniform cuts over longer production shifts.
The “Time-to-First-Cut” Reality: Separating Hobby Toys from Real Revenue Machines
Optimized Version
“Time-to-First-Cut” (TTFC) is the time from unboxing a machine to producing your first usable part. Hobby-class machines often market heavily around this, pairing proprietary, simplified software with a “cut within an hour” promise. That ease of entry is real—but it can also cap your ceiling. These plug-and-play ecosystems typically don’t offer the integration or automation you need for a professional CAD-to-CAM workflow, which means more manual setup and tweaking on every job.
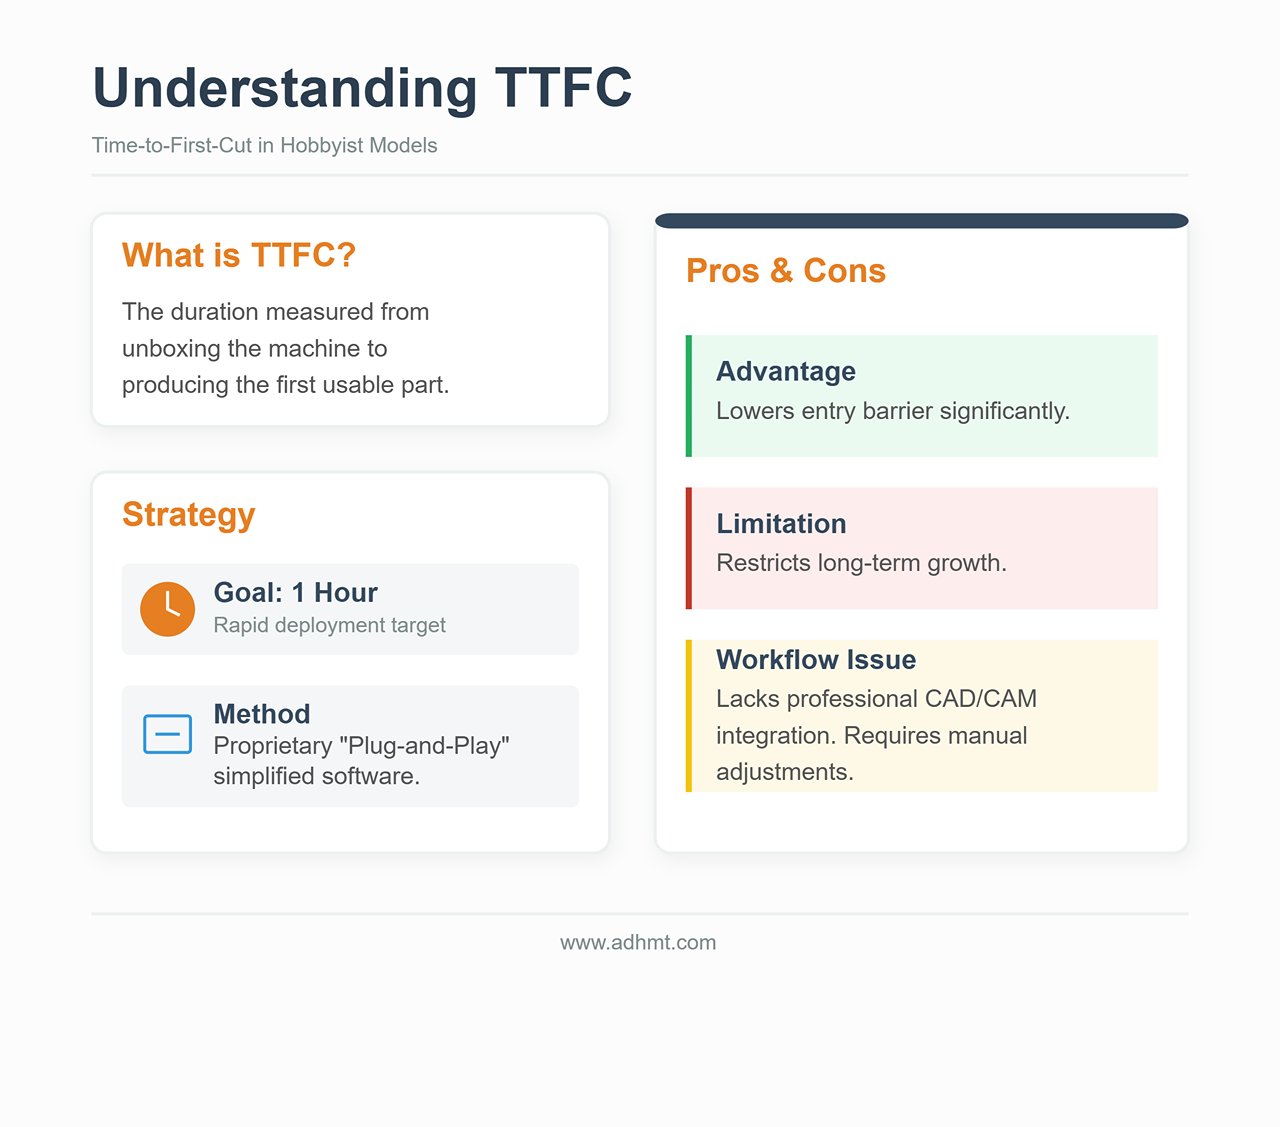
A true revenue-producing machine isn’t defined by TTFC—it’s defined by how cleanly it slots into a real production environment. Industrial-grade systems may require more upfront work (exhaust compliance, chiller setup, safety interlocks), but once they’re dialed in, “Time-to-Second-Cut” is effectively zero. That kind of efficiency depends on software compatibility that enables batch jobs, repeatable accuracy, and little to no recalibration between runs.
A machine can have a great TTFC and still be the wrong tool for production if it lacks rigidity or runs on a fragile software stack. Real ROI comes from throughput, consistency, and tight tolerance control—advantages that matter long after the novelty of unboxing wears off.
If you’re optimizing a professional workflow, reviewing the technical specs or downloading the available brochures is a practical way to understand the configurations—and the integration requirements—behind higher-volume output.
Phase 1: The Hard Filters (Eliminate 90% of Machines Up Front)
Most buyers begin by comparing wattage and price. That’s also the quickest way to end up with an expensive paperweight. The most important factors in choosing a laser cutter often have little to do with headline specs—and everything to do with the real-world constraints of your workspace.
Before you look at a single brand, apply a set of “hard filters.” These are binary constraints: if a machine fails any one of them, it’s not a contender—it’s a liability. Use these filters and you’ll remove roughly 90% of the market, leaving only the machines that can actually operate safely and effectively in your environment.
The Ventilation Veto: No Outdoor Exhaust Path, No CO2 (So Here’s What’s Left)
The first constraint is the air itself. Laser cutting is a thermal process that vaporizes material. When you cut wood, acrylic, or leather, you’re not just making dust—you’re releasing volatile organic compounds (VOCs), carbon monoxide, and a range of carcinogens. And if you cut PVC (don’t), you generate hydrochloric acid gas that can seriously damage your lungs and corrode the machine’s electronics in a matter of weeks.
The Non-Negotiable Rule: If you can’t run a 4-inch or 6-inch duct from the machine to the outdoors, you can’t buy a CO2 laser for production work.
Many manufacturers sell “fume extractors” or recirculating filtration units as a workaround for rooms with no windows. For a hobbyist engraving the occasional coaster, they can be fine. For a production shop, they’re a costly trap.
- The Saturation Issue: Cutting acrylic and wood loads up HEPA and activated-carbon filters fast. In a production setting, you may need to replace expensive cartridges weekly to keep the air safe. That can add thousands of dollars a year to operating costs.
- The Physics of Airflow: Recirculating units rarely deliver the cubic-feet-per-minute (CFM) airflow needed to keep optics clean. Without strong negative pressure vented outdoors, smoke hangs inside the cabinet and settles on mirrors and lenses. That degrades beam quality, reduces cutting performance, and can crack expensive optics.
If you don’t have a path to vent outdoors, your only realistic options are low-power diode lasers or fiber lasers used strictly for metal marking—such as the Single Table Fiber Laser Cutting Machine—which help you maintain safer air conditions and more dependable airflow.
The Electrical Surprise: Why a 110V Outlet Can Crush Your Production Speed
The second constraint is electrical capacity. In North America, a standard 110V/15A residential outlet has a theoretical maximum of 1,800 watts. But electrical code and safety standards cap continuous loads at 80%—about 1,440 watts.
New buyers often see a laser’s rating—for example, a “100W” laser tube—and assume it easily fits within that limit. That confuses output power with power consumption. A laser cutter is a system, not a single part.
- The Total Load: You’re not only powering the laser source. You’re also running the stepper motors, controller, water chiller (mandatory for glass tubes), air-assist pump, and exhaust fan.
- Voltage Sag: If the chiller’s compressor kicks on while the laser is firing at high power, that surge can briefly pull the voltage down on a shared 110V circuit.
If your shop only has standard residential 110V outlets and you can’t add a dedicated circuit, your options narrow fast. Running a high-wattage machine on a shared circuit invites “brownouts,” where laser output fluctuates—leading to cuts that don’t fully penetrate and engraving depths that vary from piece to piece.
The Hard Rule: If you can’t install a dedicated 20A circuit or a 220V line, cross high-power industrial CO2 platforms and large-format fiber lasers off your list. You’re effectively limited to desktop units or entry-level floor models where the chiller and exhaust are integrated or designed for low draw.

The Bed-Size Trap: Why “Bigger” Often Means “Slower” and “Less Precise”
Marketing would have you believe a 48″ x 36″ bed is automatically better than a 24″ x 12″ bed because it offers “more potential.” In a real shop, potential doesn’t pay the bills—throughput does.
Big beds need big gantries (the bridge that carries the laser head). Big gantries are heavy.
- Inertia vs. Detail: A heavy gantry takes more force to accelerate and decelerate. When you’re engraving fine text or detailed graphics, the head may change direction thousands of times per minute. Larger, heavier machines struggle to do that quickly without vibration—often called “ringing” or “wobble”—which shows up as ripples or waviness in the finished lines.
- The Speed Penalty: To stay accurate with a heavy gantry, the machine often has to run slower. A smaller machine with a lighter gantry can frequently engrave a batch 30% faster than a larger one simply because it can ramp up and slow down more quickly between moves.
The Hard Rule: Don’t buy a bed size for “someday” jobs. If 95% of your work fits on a 12″ x 20″ sheet, a 4′ x 8′ machine will likely hurt your business: it eats more floor space, draws more power, and often produces lower-quality engraving at a slower pace. Only step up to a large bed if cutting full sheets is your primary revenue driver.
Material Reality: Why Your Client’s Materials Dictate the Laser Source (CO2 vs. Fiber vs. Diode)
Ultimately, you can’t pick a laser source based on budget—you have to pick it based on physics. A laser’s wavelength determines which materials it will interact with. No amount of wattage can compensate for the wrong wavelength.
- CO2 Lasers (10,600 nm): The maker-world workhorse. This wavelength is strongly absorbed by organic materials.
- Must-haves for: Wood, acrylic (clear and colored), leather, paper, glass (engraving only).
- The Hard Filter: If your customers need clear acrylic trophies or architectural models, you must buy a CO2 laser. A fiber or diode laser will pass through clear acrylic without leaving a mark.
- Fiber Lasers (1,064 nm): The industrial standard for metal.
- Must-haves for: Stainless steel, aluminum, brass, copper, titanium.
- The Hard Filter: If your business model depends on cutting metal parts, a CO2 laser is the wrong tool. While high-power (150W+) CO2 lasers can cut thin metal with oxygen assist, they’re slower and produce poorer edge quality than even an entry-level fiber laser. And if you need to engrave clear plastics or wood, a fiber laser won’t help—it will scorch wood uncontrollably and often won’t mark clear plastics at all.
- Diode Lasers (450 nm): In the visible blue-light range.
- Must-haves for: Tight budgets and maximum portability.
- The Hard Filter: Diode lasers absorb poorly in clear acrylic (blue light largely passes through) and are painfully slow for cutting anything thicker than 3mm plywood. If your business depends on throughput or cutting thicker stock, rule out diode lasers immediately.

Before you move on to the specific machine recommendations in the next section, write down your three core materials. If they’re metal, you need fiber. If they’re clear acrylic and wood, you need CO2. There’s no single crossover machine that does both perfectly—unless you’re prepared to pay about as much as a small house.
Phase 2: The Software Dealbreaker
Most buyers fixate on tube wattage and bed size, treating the control software as an afterthought—just something that comes in the box. That’s the costliest mistake you can make. In a professional shop, the hardware is only as capable as the software running it. A 150W CO2 laser paired with clunky, closed-loop software isn’t a tool—it’s a bottleneck.
Before you commit to a machine, audit the digital ecosystem it forces you into. If the software workflow is broken, the machine’s speed doesn’t matter.
Why “LightBurn Compatible” Is Non-Negotiable for Professional Work
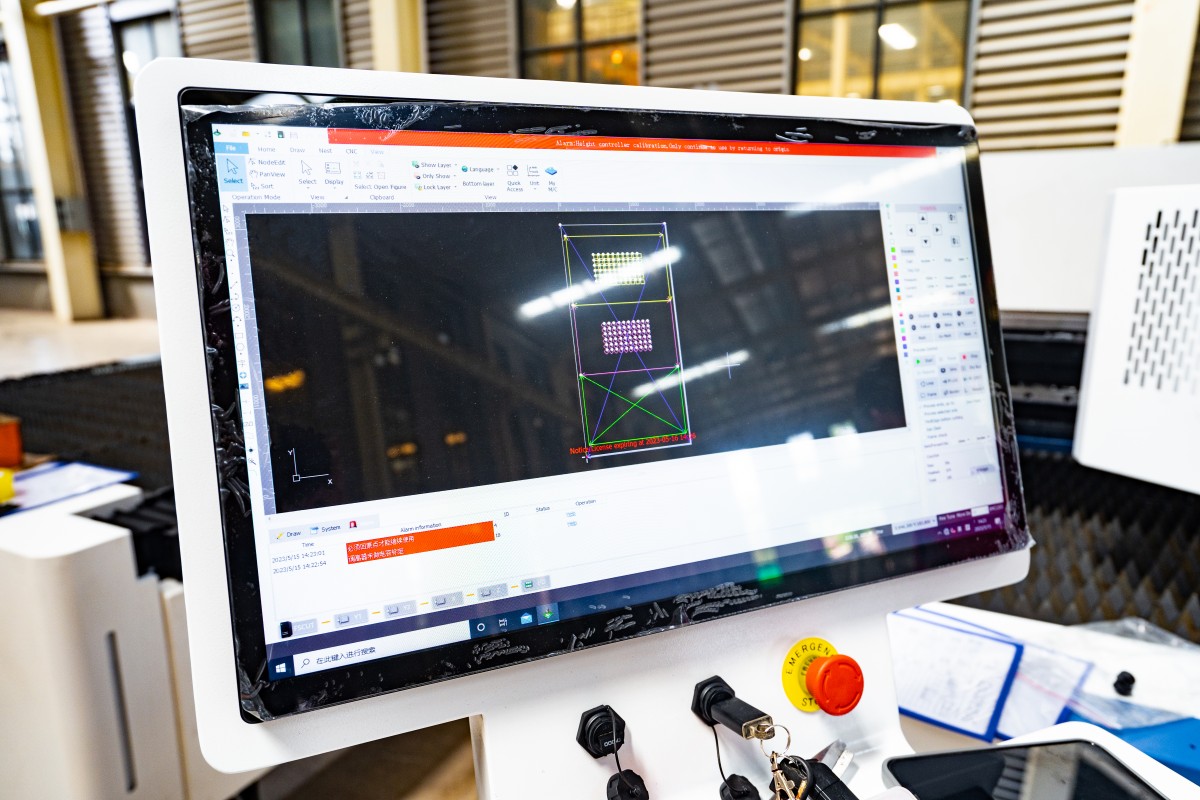
In the laser world, LightBurn has grown from a handy third-party app into the de facto operating system for professional fabrication. It serves both as CAM (Computer-Aided Manufacturing) software—where you set speeds, power, and toolpaths—and as the machine control interface.
For a workshop, “LightBurn compatibility” isn’t a nice-to-have—it’s a strategic asset for three reasons:
- Labor Portability: LightBurn standardizes the interface across very different machines. It supports Ruida, Trocen, TopWisdom, and GRBL controllers. Train an operator on a basic diode laser and they can carry those skills to an industrial CO2 flatbed or a galvo fiber marker without relearning the entire workflow. Buy a machine locked to proprietary software and you increase training costs with every new hire.
- Standardized SOPs: Scale requires Standard Operating Procedures. When your whole fleet runs on one platform, you can build a unified material library—save proven settings for “3mm birch plywood” or “anodized aluminum” and push them to any machine in the shop. Proprietary software forces fragmented libraries, raising the odds of operator error and wasted material.
- The “Bus Factor”: If a closed-ecosystem manufacturer goes under, stops maintaining its software, or changes pricing, your hardware can become obsolete overnight. A machine with a standard controller (like a Ruida 6442) running LightBurn is far more future-resistant—the hardware isn’t tied to the manufacturer’s survival.
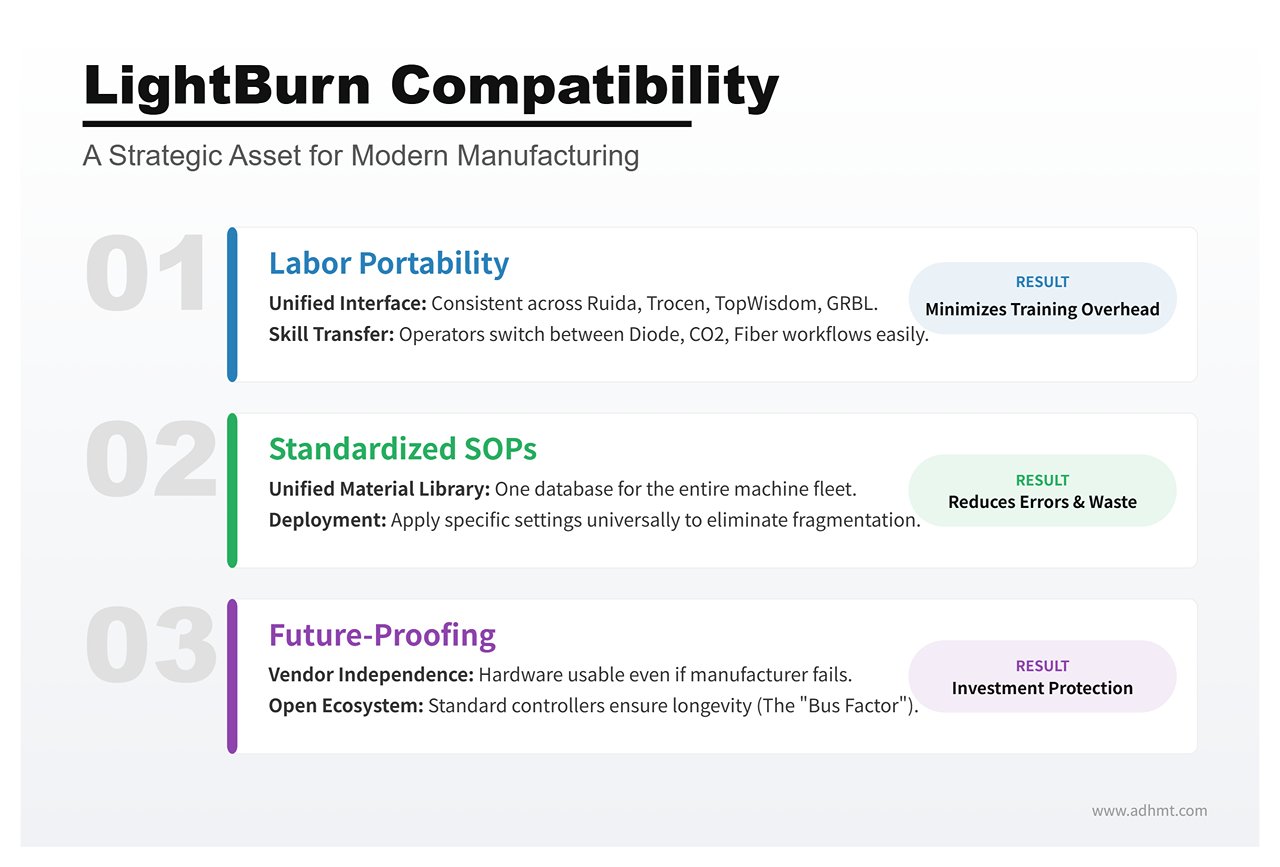
If a machine manufacturer doesn’t support LightBurn, they’re effectively asking you to stake your production line on their in-house software team. For professional work, that’s a gamble you should almost never take.
The Hidden Cost of Proprietary Ecosystems: Internet Requirements and File Limits
Consumer-grade laser brands often pitch their proprietary software as “user-friendly,” but that simplicity often hides a walled-garden design built to monetize how you use the machine.
The biggest risk in these ecosystems is cloud dependency. Some machines require an active internet connection just to process design files. The software uploads your vector data to the manufacturer’s servers, generates the G-code remotely, then sends it back to the machine. For a hobbyist, that’s an annoyance. In production, it’s a serious liability. If your ISP goes down, your line stops. If the manufacturer’s servers hiccup, your deadlines slip.
On top of that, proprietary ecosystems often impose artificial restrictions on file handling. You may run into:
| Issue | Description |
|---|---|
| File Lock-in | No ability to export project files in standard formats (DXF, SVG), effectively trapping your intellectual property inside their system. |
| Subscription Paywalls | Core productivity features—like array nesting (automatically packing multiple parts onto a sheet to reduce waste) or vector tracing—may sit behind a monthly “Premium” subscription. |
| Privacy Risks | For shops handling sensitive client prototypes or IP, uploading designs to a third-party cloud for processing can violate standard NDA practices. |
Professional hardware should run locally. You should be able to plug in a USB cable (or load a file from a USB drive) and cut regardless of your Wi‑Fi status.
Workflow Efficiency: Can You Import CAD/Illustrator Files Without a Headache?
Efficiency comes down to the time between finishing a design and hitting “Start” on the laser. That gap is largely determined by file compatibility.
Your design team is probably working in Adobe Illustrator, AutoCAD, SolidWorks, or Rhino. Your laser software needs to connect those tools to the machine’s motion controller directly—without forcing you into a third “translator” program.
A professional workflow depends on true direct-import support. You should be able to drop an AI, PDF, DXF, or SVG straight into the control software and have it read the vectors accurately.
- Layer Mapping: The software should automatically translate colors in your design file into cut settings (e.g., red lines = cut, blue lines = engrave).
- Native Editing: Minor tweaks—closing an open shape, welding text, or offsetting a path for kerf compensation—should be doable inside the laser software. If you have to jump back to Illustrator just to move a hole 2 mm to the left, your workflow is hemorrhaging time.
If a machine makes you convert vector files into a proprietary raster format—or forces you through a clunky import wizard every time you revise a design—it fails the efficiency test. The goal is a clean pipeline: Design → Import → Cut. Anything else is friction.
Phase 3: The Scenarios (Find Your Specific Situation)
Most buying guides miss the mark because they treat a hobbyist in an apartment and a sign shop in a warehouse like the same customer. They’re not. A machine that’s perfect for one can be a liability for the other.
Now that we’ve established the technical “hard filters” in the previous section, we can apply them to the three most common user scenarios. Find yourself below to see which machines actually make the cut.
Scenario A: The “Side Hustle” Desktop Units (Limited Space, Maximum Ease of Use)
This scenario fits if you’re working out of a spare bedroom or small studio, have limited ventilation options, and value “time-to-first-cut” over raw horsepower. You need a machine that looks like a printer—not a science project.
The “Plug-and-Play” Contenders: Glowforge vs. xTool P2 vs. Gweike Cloud
The Glowforge Pro defined this category for years. Its “walled garden” approach is a lot like Apple’s ecosystem: incredibly easy to use, excellent camera alignment, and a Proofgrade materials system that eliminates the guesswork on power settings. The trade-off is that it needs an active internet connection to run. If your Wi‑Fi drops, production stops.
The xTool P2 has become the leading challenger. It rivals the Glowforge on ease of use (camera-based positioning, autofocus) while avoiding the “walled garden.” It supports LightBurn, works fully offline, and offers a riser base for engraving taller items—something the Glowforge handles poorly.
The Gweike Cloud is the value pick. You get similar 50W CO2 power in a desktop-sized package for significantly less money. The hardware is robust, but the software experience isn’t as refined as what you’ll find with its main competitors.
The Trade-off: Paying for Convenience vs. Repairability
The hidden cost of desktop machines is repairability. To keep these units sleek and “safe,” manufacturers seal components inside enclosed housings.
If a laser tube fails in a Glowforge, you typically can’t replace it yourself; in many cases, the entire unit has to be shipped back to the manufacturer. That can mean weeks of downtime. The xTool P2 and Gweike Cloud sit in the middle: users can replace tubes and mirrors, but the work is tighter and more awkward than on a larger industrial machine. You’re paying for a small footprint—make sure your business can absorb potential downtime and/or the cost of proprietary parts.
Scenario B: The “Garage Production” Workhorses (Maximum Power, Lower Cost)
This scenario is for the maker with dedicated garage space, a dryer vent for exhaust, and a willingness to get hands-on. You want the most wattage per dollar and a large cutting bed (20″x28″ or bigger).
The OMTech & Monport Approach: High Capability, High Maintenance
Brands like OMTech and Monport import industrial “China Blue/Red” CO2 lasers and sell them at aggressive price points. An 80W OMTech often costs less than a 45W Glowforge. These machines are tanks: they use industry-standard Ruida controllers (fully compatible with LightBurn), common off-the-shelf parts you can source on Amazon, and large pass-through doors for oversized sheets.
That said, quality control can be inconsistent. You’re not paying for a polished consumer experience—you’re paying for raw steel and glass.
The “Tinkerer’s Tax”: Assessing Your Ability to Align Mirrors and Swap Controllers
The “Tinkerer’s Tax” is the time you’ll spend getting the machine dialed in. Unlike desktop units, these lasers often arrive with mirror alignment knocked out during shipping. You need to be comfortable loosening locknuts, firing test pulses, and adjusting the beam path.
If high-voltage electronics or mechanical alignment genuinely intimidate you, don’t buy these machines. But if you’re comfortable with a wrench and a multimeter, they deliver some of the best ROI you’ll find anywhere in the industry.
Mandatory Upgrades: Chillers and Air Assist You Need to Budget for Right Away
The “sticker price” on these units is misleading. The included “water pump” is typically a basic aquarium pump that can’t keep an 80W tube properly cooled during long cuts—leading to overheating and shortened tube life. The included “air assist” is often just a weak fan that doesn’t clear smoke effectively, which leaves you with charred edges.
To make an OMTech or Monport truly production-ready, you should plan to spend an additional $800–$1,000 immediately on:
- A CW-5200 active chiller (refrigerated cooling).
- A real air compressor (for cleaner cuts).
- An upgraded inline exhaust fan.

Scenario C: The Professional Workshop (Speed, Reliability, & US Support)
This scenario is for businesses where the laser is a primary revenue driver. If the machine goes down, you’re losing money. You need speed, accuracy, and a phone number you can call when something breaks.
Stepping Up to Thunder Laser, Aeon, and Boss: What an Extra $4K Actually Gets You
Moving from an OMTech to a Thunder Laser Nova, Aeon Mira, or Boss Laser is a major price jump—often $4,000 to $6,000 more for comparable wattage.
You’re not paying for more raw power; you’re paying for servo motors (instead of steppers), linear rails, and—in higher-end configurations—RF (radio-frequency) metal tubes. These components last longer and maintain calibration better under 24/7 use. Tolerances are tighter, wiring is cleaner, and the safety interlocks are industrial-grade.
The Speed Factor: Why Raster Performance Matters More Than Cutting Power
Beginners obsess over cutting power (watts). Pros obsess over raster speed (inches per second).
If your business engraves tumblers, leather patches, or slate coasters, the laser head has to sweep back and forth thousands of times. A budget stepper setup may top out around 500 mm/s and produce “ringing” (wavy, wobbly lines). A Thunder Laser or Aeon with hybrid servos can run at 1000 mm/s+ with crisp, razor-sharp results—effectively doubling your daily throughput. In a production shop, speed is the metric that matters.
Local Support: The “Insurance Policy” That Saves You From a 3‑Week Parts Delay
The single biggest advantage in Scenario C is U.S.-based support.
When a controller board dies on a no-name import, you’re usually left combing through forums or emailing a factory in China—then waiting weeks for a replacement. Brands like Thunder, Aeon, and Boss keep U.S. warehouses stocked with parts and have English-speaking technicians who can troubleshoot with you over a video call.
For a hobbyist, waiting three weeks for a part is frustrating. For a professional shop, it can be catastrophic. That extra $4,000 is essentially an insurance premium against downtime—and radio silence.
Phase 4: The Final Reality Check Before You Order
You’ve got your shortlist. You’ve got your budget. Your cursor is hovering over “Add to Cart.” Stop.
There’s a world of difference between a machine that cuts demo files at a trade show and one that keeps a business running for the next five years. That gap rarely shows up on a spec sheet—it shows up in the day-to-day friction of actually using the thing. Before you commit your money, run your top pick through three final filters. These are the fail-safes that separate a profit-producing tool from a heavy, expensive garage decoration.
Maintenance Access: The 60‑Second Check That Can Save You a Week of Lost Work
Laser maintenance isn’t a “someday” project—it’s a weekly necessity. Vaporized glue and wood resins collect on your optics fast: roughly 1–2 grams per week. If cleaning your mirrors requires 30 minutes of teardown, you’ll start skipping it. And once you skip it, that residue bakes into the lens coating, costs you ~30% power, and eventually cracks the optic.
The Test: Ask the vendor or watch a real user video. Can you access, remove, wipe, and reinstall Mirror 1, Mirror 2, and the focus lens in under 60 seconds total?
If not, walk away.
- Mirror 1 (Tube End): You want a side access door. Ideally, you can twist a retaining ring and pull the mirror in under 15 seconds. (OMTech and Gweike usually pass; Glowforge often fails by hiding the optic behind panels.)
- Mirror 2 (Gantry): Look for a flip-top cover. You should be able to clean it with a Q-tip without removing the mount. If you have to unbolt ventilation ducting just to reach it (common on older Monport designs), you’re paying a “maintenance tax” every Friday.
- Mirror 3 & Lens (Laser Head): This is the make-or-break area. You should be able to lower the bed, remove the nozzle ring, and have the lens drop safely into your hand in under 20 seconds. Pro Tip: When reassembling, make sure the lens goes back in “belly up” (convex side facing up). If you need a hex key just to access the lens, it fails the test.

The “Buy Nice or Buy Twice” Decision Matrix
A $3,000 machine is never just $3,000—it’s a down payment on future repairs. An $8,000 machine, on the other hand, often costs less over a five-year horizon. This matrix reveals the Total Cost of Ownership (TCO) hiding behind the sticker price.
Identify the column that best matches the machine on your shortlist:
| Dimension | The Budget Build (Scenario B) | The Pro Workhorse (Scenario C) |
|---|---|---|
| Upfront Cost | $2,000 – $4,000 | $6,000 – $10,000 |
| Tube Life | 1k–2k hours (Glass CO2) | 10k+ hours (RF Metal/High-end Glass) |
| Est. Downtime/Year | 15 days (waiting for parts) | 2 days (local support/better QC) |
| Weekly Maintenance | 2 hours (manual alignment) | 30 mins (sealed optics/better rails) |
| Replacement Cost (Year 4) | $1,000+ (New tube + PSU) | $0 (Long-life source) |
| Resale Value | 40% of original price | 70% of original price |
| 5-Year TCO | $19,000+ (inc. lost billable hours) | $7,000 (low consumables) |
If you’re running a hobby shop, the Budget Build is fine—your time is “free.” If you’re running a business, the downtime from a “cheap” machine will wipe out the price difference versus the “expensive” one within the first 18 months.
Checklist: Be Ready to Cut Within 48 Hours of Delivery
The most dangerous time for a laser owner is the first week. Without the right supplies, the machine sits idle while your return window ticks away. And if you don’t verify the optics immediately, any shipping damage becomes your problem.
Follow this timeline so you’re operational—or ready to send back a lemon—right away.
Day 0: The Pre-Arrival Run (2 Hours)
- Fluids: Buy 2 gallons of distilled water (for the chiller) and 90% isopropyl alcohol (for optics).
- Optics Kit: Have lens paper and thermal paper (receipt paper) on hand for alignment testing.
- Power: Confirm a dedicated 20A circuit (110V/220V depending on the unit). Sharing a circuit with a fridge or compressor will trip breakers and wreck cuts.
Day 1: Unbox & Inspect (4 hours)
- The Shake Test: Before you fill the chiller, inspect the laser tube for internal cracks. If you hear glass tinkling when you gently rock the tube, refuse the delivery.
- The Leak Test: Hook up the water, run the pump, and wait 30 minutes. Check the tube ends and the bottom of the chassis.
- The 60-Second Clean: Perform the maintenance check you researched in Step 1.
- Alignment: Use thermal paper to verify the beam path at all four corners of the bed.
Day 2: Validation (2 hours)
- The Frame Test: Run a 10 mm/s vector cut on wood at 90% power.
- The Output: Edges should come out golden-brown, not charred black. The kerf should be vertical, not angled.
- The Stress Test: Run the machine for 3 hours. Watch the temperature (keep it below 22°C/71°F). If it overheats or drifts out of focus, send it back.
The Final Cut
At the start of this guide, we asked whether you’re building a workshop or simply buying a tool. The difference isn’t the brand name stamped on the chassis—it’s the owner’s level of preparation.
By following this four-phase framework, you didn’t just shop for a laser—you set yourself up to succeed. You clarified your material requirements, calculated the power you need, locked in your safety protocols, and uncovered the hidden costs of ownership. You’re no longer hoping for a good machine; you’ve engineered a smart purchase.
The research is done. The checklist is ready. Now it’s time to cut. And if you’d like hands-on help matching your workflow to the right technology, feel free to contact us for tailored laser system guidance.

VI. FAQ
1. Can laser cutters cut metal?
Yes—some laser cutters can cut metal, but it depends on the laser type and power. Fiber lasers and high-power CO2 systems can typically cut a range of metals, including stainless steel, aluminum, and copper. For thicker sheets or more demanding applications, industrial fiber machines such as the Single Table Fiber Laser Cutting Machine are recommended.
2. What materials can a CO2 laser cut?
Common materials include wood, acrylic, leather, fabric, paper, and certain plastics. However, CO2 lasers generally aren’t suitable for cutting metal unless they’re very high power and specifically engineered for metal cutting. They’re also not recommended for cutting PVC or other materials that release toxic fumes when heated.
3. How precise are laser cutting machines?
One of the biggest advantages of laser cutting machines is their precision. High-quality laser cutters can produce extremely fine details, with tolerances as tight as 0.001 inches (0.025 mm). Actual precision depends on factors such as beam quality, machine rigidity and stability, and the accuracy of the motion-control system.